Direct Factory Solutions
Precision HMI & Complementary Embedded Hardware
Engineered to survive corrosive coastal air, high moisture, and intense duty cycles. Every membrane keypad and electronic sub-assembly undergoes rigorous continuity, insulation, and environmental testing.
Engineering Whitepaper
Overcoming Humid, Marine & Tropical Challenges in the Jamaica Market
A technical evaluation on design criteria, membrane overlay polymers, switch contact reliability, and compliance required for industrial operations across Kingston, Montego Bay, and regional extraction facilities.
Procuring Human-Machine Interfaces (HMIs) and membrane control switches for deployment across the Caribbean basin—specifically within Jamaica's maritime, agricultural processing, bauxite mining, and hospitality automation infrastructures—demands uncompromising material science. Equipment deployed in port infrastructure at Kingston Wharves or food & spirits production lines around Saint Catherine faces a combination of airborne salinity, high relative humidity (regularly exceeding 85%), ambient temperature cycling, and ultraviolet radiation. Conventional tactile panels with inferior PET substrates or porous adhesives suffer rapid trace oxidation, silver migration, and overlay delamination.
As a verified electronics and HMI manufacturer, Shenzhen Mivo Electronics Co., Ltd. builds CE-certified membrane panels utilizing premium Autotype Autotex/Autoflex polyester films, antimicrobial textures, and selective conductive silver traces passivated with protective carbon or dielectric ink coatings. When coupled with perimeter gasket barriers rated up to IP67, our membrane keypads isolate internal stainless steel tactile metal domes from corrosive external atmospheres, ensuring operating lives exceeding 1,000,000 actuations without loss of tactile response or contact resistance degradation.
| Performance Parameter | Standard Commercial Membrane Panel | Mivo Tropicalized CE Certified Membrane Panel |
|---|---|---|
| Overlay Substrate | Untreated Polycarbonate (PC) (Brittle under UV) | Biaxially Oriented Coated PET (Autotex F/V Series, UV & Chemical Proof) |
| Trace Protection & Anti-Silver Migration | Exposed Silver Ink with standard cure | Passivated Silver Ink with Carbon Overcoat & High-dielectric UV Curable Masks |
| Environmental Sealing Rating | IP40 - IP54 (Dust permeable) | Up to IP67 with closed-cell 3M 200MP / 300LSE acrylic perimeter sealing |
| Contact Resistance Stability | < 100 Ω initially, drifting fast in humidity | < 10 Ω stabilized; Gold/Nickel-plated snap domes rated > 1M cycles |
| Operating Temperature Window | -10°C to +50°C | -40°C to +85°C (Validated for enclosed Caribbean electrical cabinets) |
EMI/RFI Shielding Options
Integrated aluminum foil, copper mesh, or selective conductive grid layers protect delicate PCBA controllers from harsh industrial noise, grid instability, and high-frequency inverter interference.
Rigid Backer Integration
Support for CNC-machined anodized aluminum plates, acrylic backplanes, or directly laminated FR-4/Aluminum PCB cores, providing complete structural rigidity for harsh control room enclosures.
Tactile Response & Illumination
Engineered stainless steel metal domes with custom tactile feedback curves, integrated thin-film surface mount LEDs (0603/0805), light guide films (LGF), and dead-front graphic printing for high legibility.
Target Deployments
Localized Applications Across Jamaican Industry Sectors
Addressing operational requirements through customized human-machine interface assemblies.
Food, Beverage & Sugar Processing
Deployed in bottling lines, sugar refiners, and rum distilleries. IP66/IP67 sealed membrane surfaces resist caustic washdown fluids, high temperatures, alcohol vapor, and organic residue accumulation without graphic degradation.
Bauxite Extraction & Heavy Processing
Alumina facilities face abrasive mineral dust, vibrations, and outdoor exposure. Sealed tactile switch matrices prevent dust ingress that routinely jams mechanical pushbuttons, maintaining clear status indication via embedded LEDs.
Hospitality & Commercial Building Automation
From central HVAC controls in large Montego Bay and Ocho Rios resorts to commercial pool pumping, solar inverter interfaces, and water filtration consoles, our UV-resistant graphic overlays prevent sun-bleaching and embrittlement.
Market Dynamics
Emerging HMI & Electronics Manufacturing Trends in the Caribbean
How Jamaican procurement managers and systems integrators are adapting control systems for sustainability and efficiency.
Renewable Energy & Microgrid Expansion
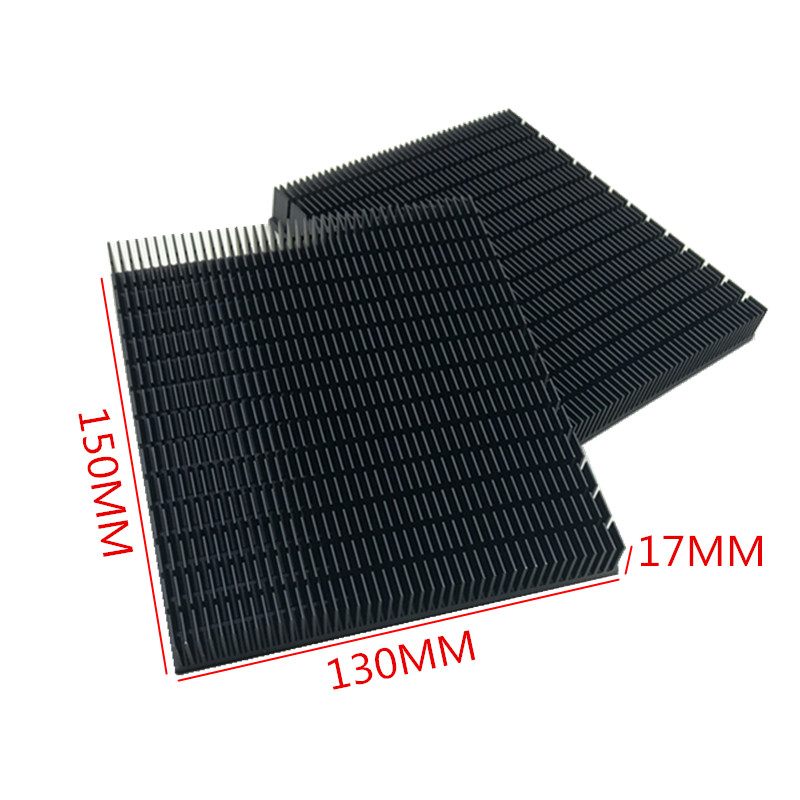
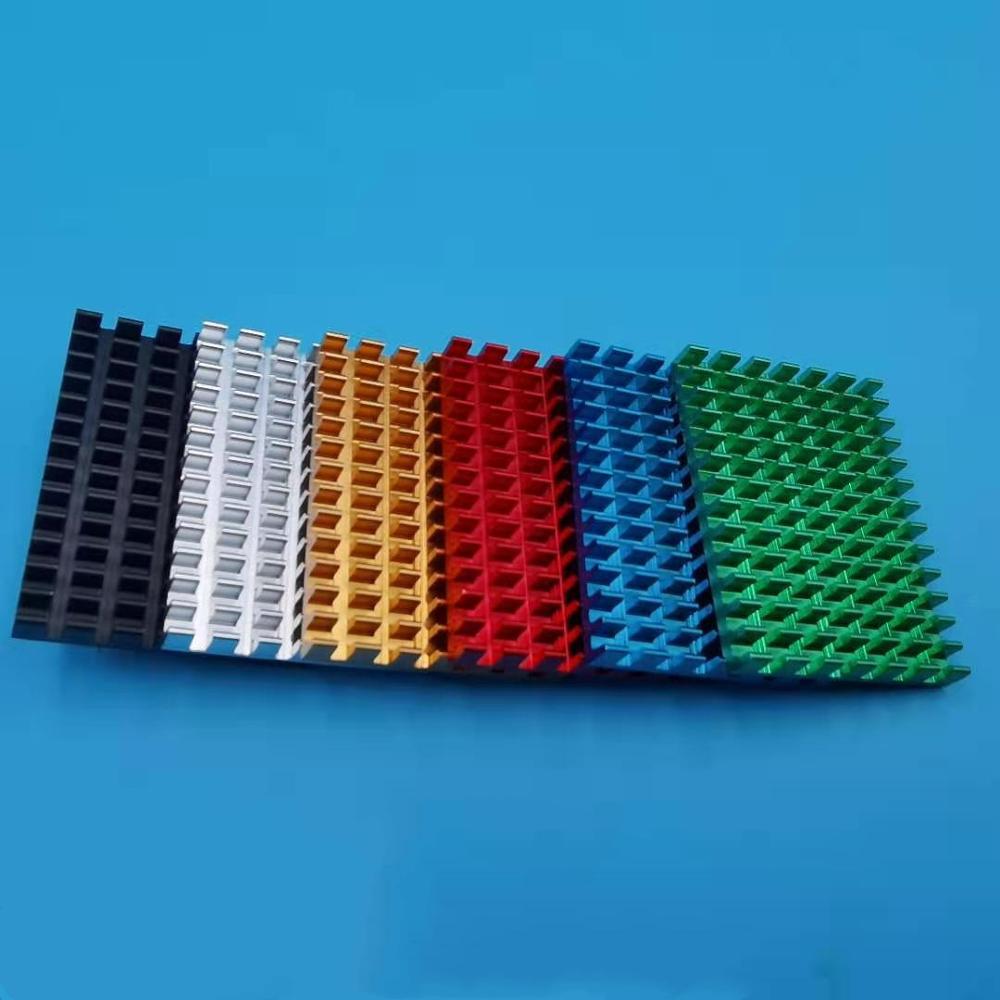
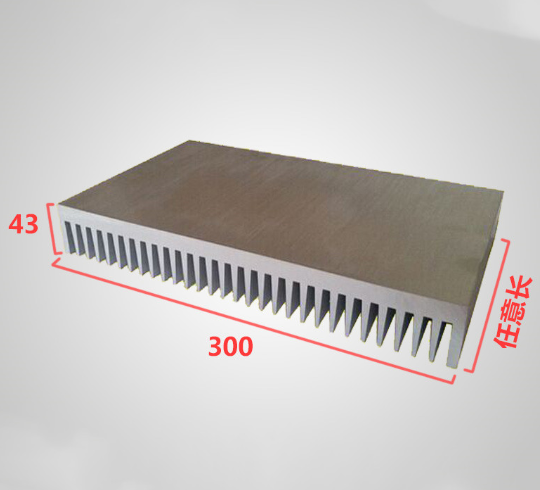
With Jamaica's aggressive transition toward wind and solar energy, outdoor-rated inverter interfaces and battery storage management displays require UV-blocking overlays and thermally conductive aluminum base heat sinks to withstand relentless solar heating.
Retrofit Over Replacement Strategy
Due to high import duties and shipping lead times on full replacement machinery, industrial plants across Kingston are actively retrofitting legacy automation consoles with custom-dimensioned, CE-certified membrane panels, extending machine longevity at a fraction of capital expenditure.
IoT-Enabled Sensor & HMI Convergence
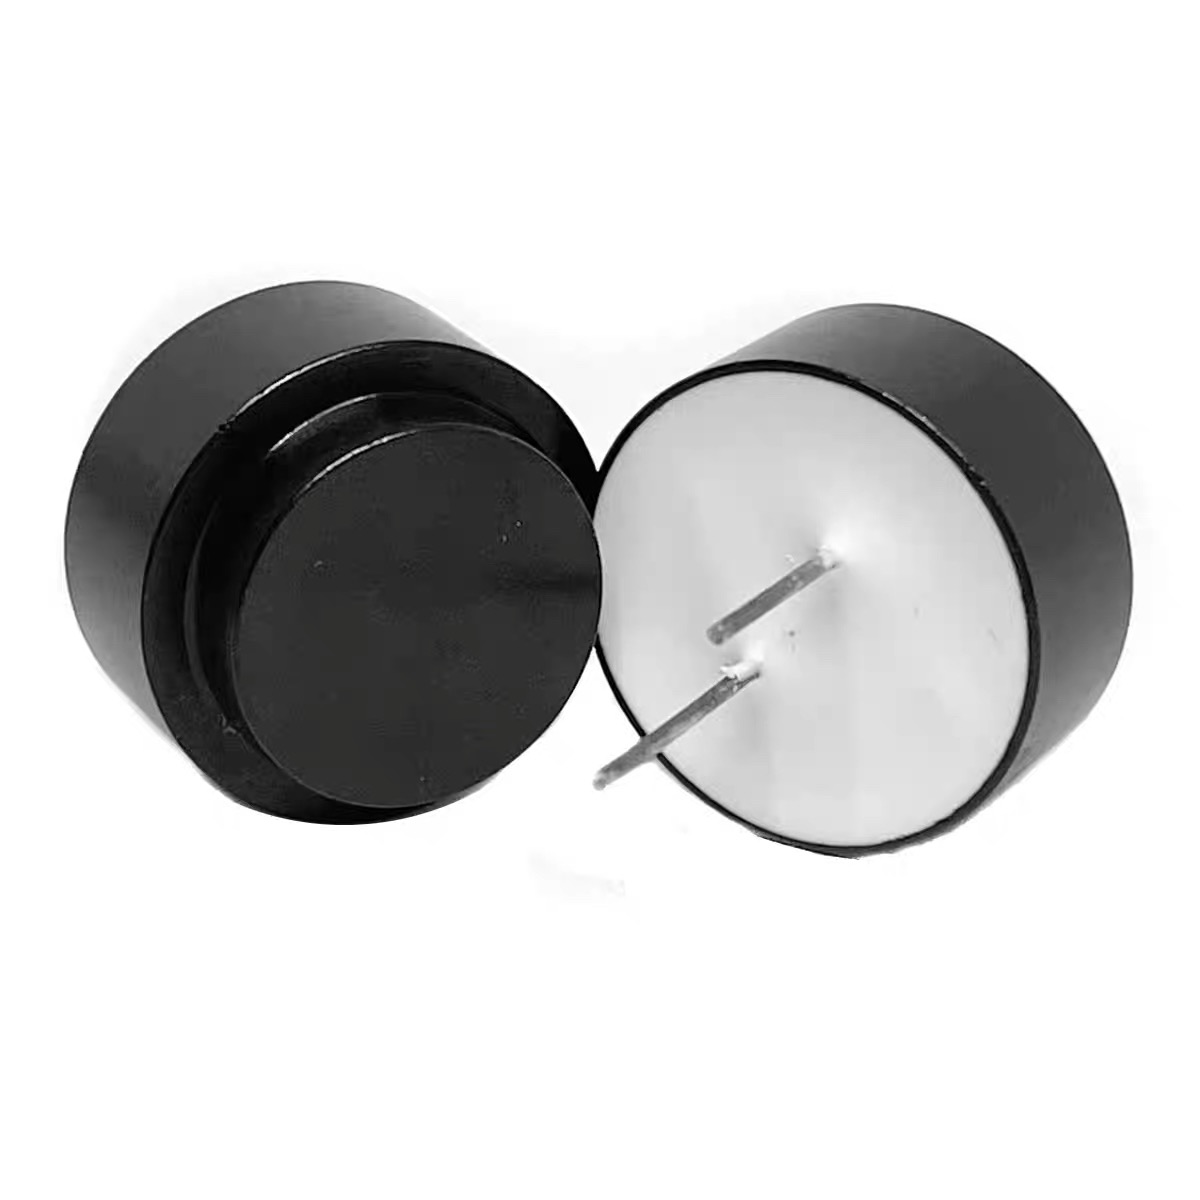
Panels are no longer standalone switches. Jamaican industrial engineering teams are integrating temperature probes (PT100/NTC), liquid leak detection loops, and ultrasonic level monitors directly through unified controller PCBA boards built to precise engineering drawings.
Manufacturer Authority
Why Engineers & Importers Partner with Shenzhen Mivo Electronics
Combining turnkey electronics assembly with precision mechanical and panel fabrication from China’s leading hardware ecosystem.
Onsite-Verified Manufacturing
Our manufacturing facility has passed verified onsite audits by third-party inspection firms and global B2B platforms. We operate with an established engineering team of 51–100 professionals focused on build-to-print execution.
Low Prototyping Barrier (From 5 Pcs)
We eliminate high startup minimums. Rapid prototyping for custom PCBA and membrane switches begins from just 5 to 10 pieces, allowing Jamaican engineering contractors to prototype without excessive front-end inventory risk.
8+ Years Verified Export History
Maintained a 4.7 / 5 buyer satisfaction rating across 8+ years of global exporting. Our transparent DFM reviews, open BOM component tracing, and explicit approval processes ensure exact alignment with technical drawings.
2016
Year Established (Verified Onsite)
4.7 / 5
Average Buyer Satisfaction Rating
5 Pcs
Low Minimum PCBA Prototype Order
100%
Electrical & Function Testing
Procurement Support
Frequently Asked Questions by Caribbean Buyers
Practical guidance on lead times, shipping, international standards, and custom tooling.
What certifications accompany your membrane switch panels and electronics?
Our membrane panels, custom PCB assemblies, and sensor modules are manufactured under strict ISO9001 quality management procedures and comply with CE directives (Low Voltage Directive and EMC compliance). Material safety data sheets (MSDS) and RoHS / REACH declarations are provided with shipments to verify non-toxic, flame-retardant, and lead-free compliance for clear customs clearance through the Jamaica Customs Agency (JCA).
How do you ensure membrane panels do not delaminate in high humidity environments?
For humid tropical climates, we avoid standard water-based adhesives. Instead, we specify industrial-grade acrylic bonding films such as genuine 3M 467MP, 3M 468MP, or 3M 300LSE designed for high-surface-energy metals and low-surface-energy powder-coated plastics. Panels feature complete internal perimeter gaskets and breathable vent channels routed into sealed back chambers to balance atmospheric pressure swings without admitting ambient moisture.
What design files do we need to submit for an accurate quotation and DFM review?
For membrane switches, please provide vector artwork files (Adobe Illustrator .AI, CorelDraw .CDR, or vector .PDF) including graphic layers, Pantone/RAL color codes, embossing zones, and window cutouts, along with a schematic/circuit pinout diagram. If you are ordering turnkey assemblies with internal controller boards, please supply Gerber files (RS-274X), a Bill of Materials (BOM) detailing manufacturer part numbers, and centroid (pick-and-place) coordinates.
What are typical production lead times and logistics routes to Kingston and Montego Bay?
Membrane switch samples and rapid PCBA prototypes typically require 7 to 12 working days once engineering drawings are frozen. Mass production runs take 2 to 3 weeks depending on material volume. Shipments to Jamaica are typically dispatched via express air couriers (DHL, FedEx, UPS) directly to Norman Manley International Airport (KIN) or Sangster International Airport (MBJ) in 4 to 7 business days, or via consolidated ocean freight to the Port of Kingston for large volume orders.
Can Mivo Electronics source obsolete or hard-to-find components for our control boards?
Yes. Leveraging our established electronics supply network in Shenzhen, we source active components, connectors, tactile switches, and discrete semiconductors directly from authorized franchise distributors. When long lead-time or discontinued components are identified on your BOM, our engineering team prepares a detailed technical cross-reference proposal for your written verification and testing before procurement.
Request an Engineering Consultation & Rapid Prototype Quote
Whether you require a custom marine-grade membrane panel, industrial heat sink profiles, or a full turnkey SMT assembly run, our Shenzhen engineering facility is equipped to assist your next project.
Get a Quote