Featured Electro-Mechanical & Sensor Control Products
Precision-manufactured electronic assemblies, tactile interfaces, thermal management units, and optoelectronic modules available for direct export to Belizean original equipment manufacturers, maintenance contractors, and automation fabricators.
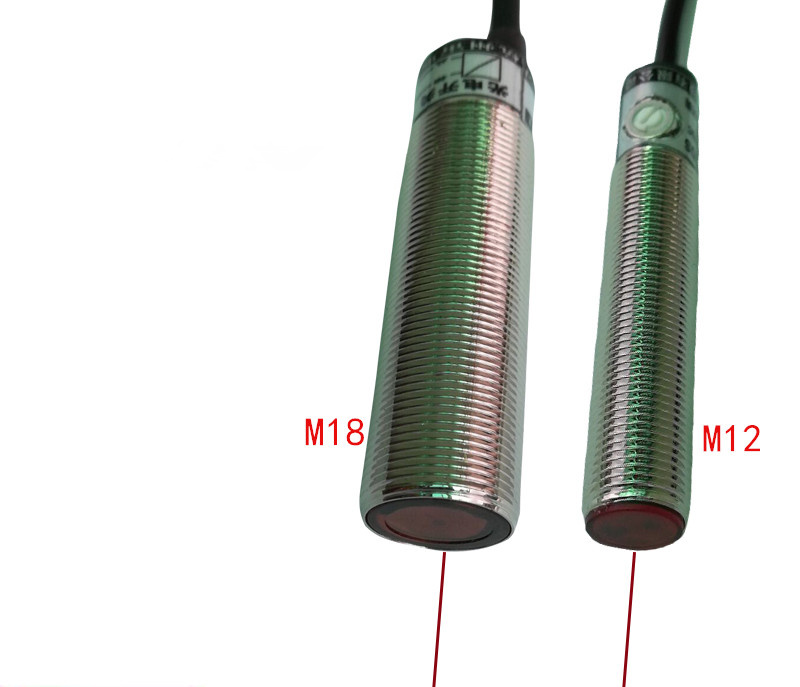
M18 Laser Sensor Visible Light Photoelectric Diffuse Reflection Infrared Ray M12 Photoelectric Switch Sensor Switching Inductor
Rugged IP67 brass-nickel housing, visible red laser emission for high-speed conveyor positioning in sugar milling and packaging.
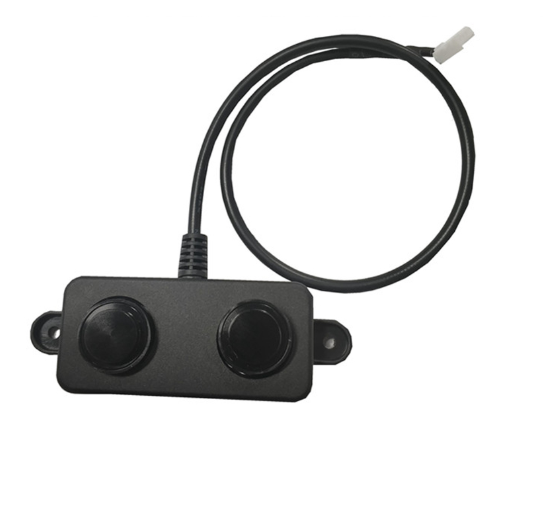
UART PWM Output Water Proof Module Waterproof Ultrasonic Distance Sensor
Sealed transducer resistant to condensation; ideal for Belize municipal canal runoff, agricultural cisterns, and water purification storage.
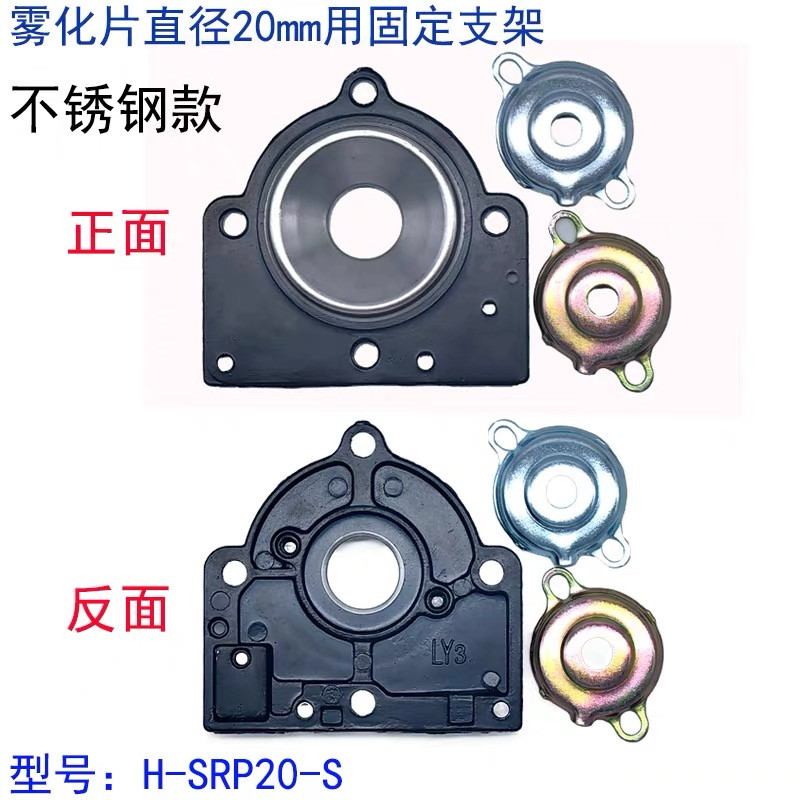
Atomizing Plate Stainless Steel Heat Sink Humidifier Accessories Atomizing Fixed Holder Aluminum Alloy Heat Sink
Corrosion-resistant 304/316 stainless steel bracket and anodized aluminum sink designed for agricultural humidification and resort climate control.
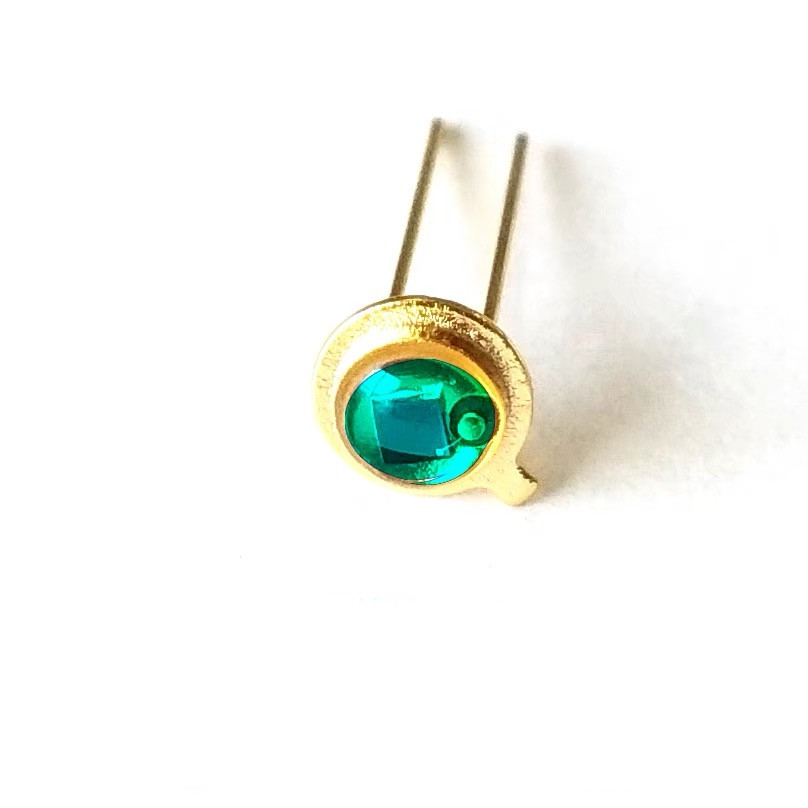
Metal Shell TO46 Package SG-PIN46MR-V High Speed Photodiode Silicon Photocell 450NM Silicon Photodiode SGPIN46MR-V
Hermetically sealed TO-46 metal canister, 450nm spectral response for optical water testing, fluorescence measurement, and laboratory instrumentation.
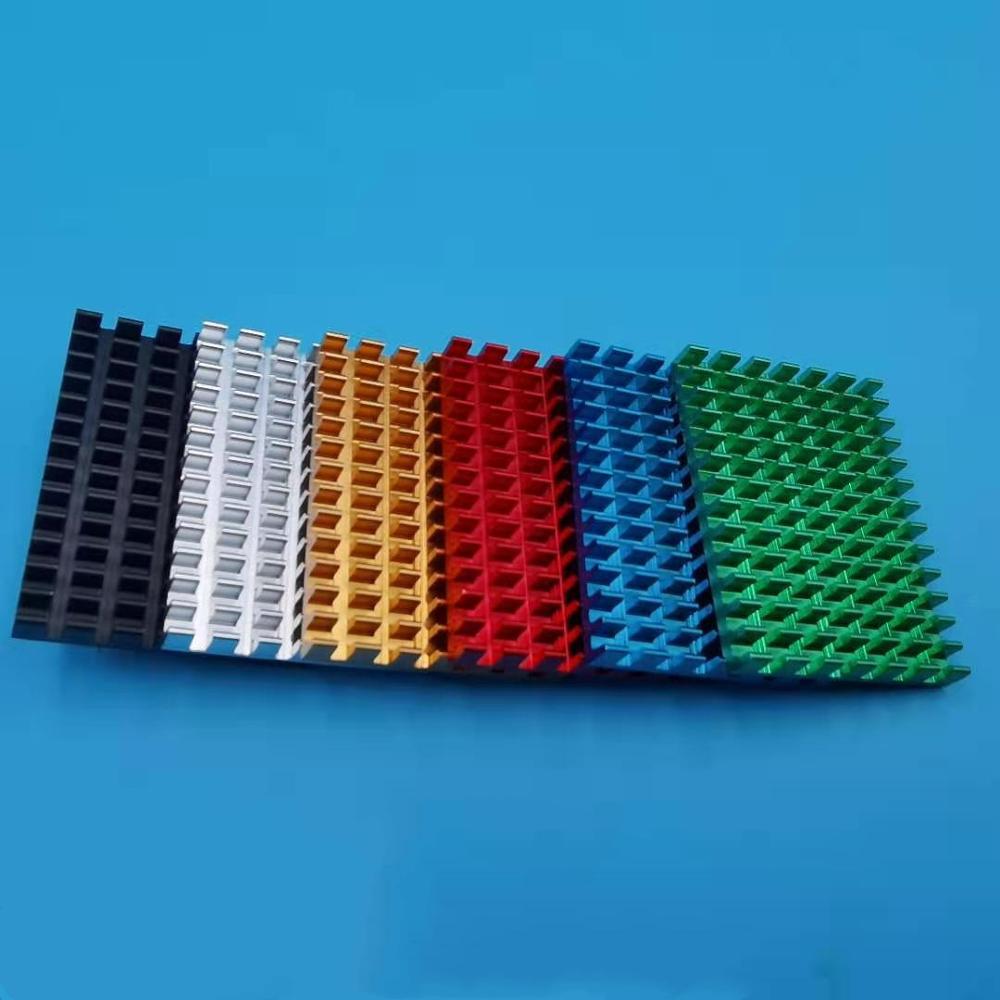
30*40*5MM Aluminum Profile Heat Sink Chip IC CPU Router Memory PCB Board Electronic Cooler
Precision-extruded 6063-T5 aluminum radiator with high thermal dissipation fins, critical for preventing micro-controller overheating in tropical ambient heat.
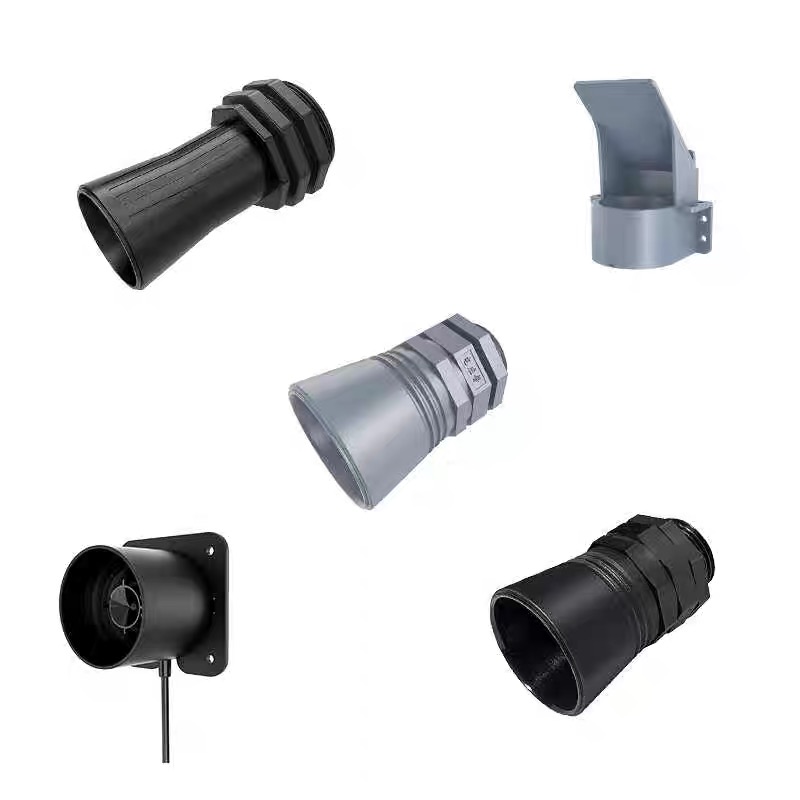
Ultrasonic Sensor Level Meter Down-well Ranging Water Level Measurement Module Water Level Measure tank of Sewer Pipe Network
Chemical and methane resistant enclosure, non-contact level telemetry for wastewater collection, cisterns, and flood warning stations.
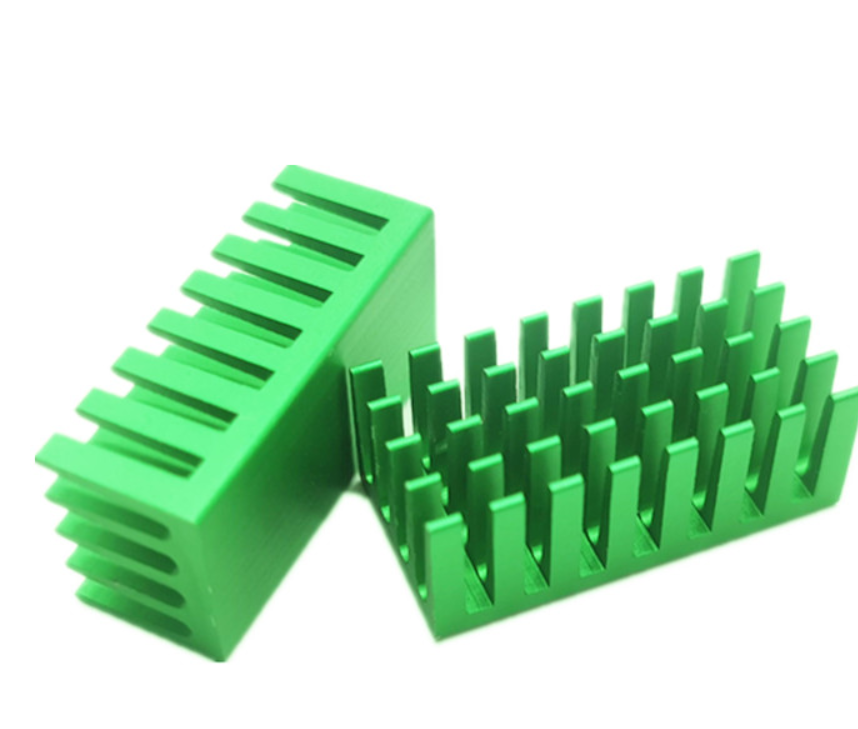
Electronic Chip Radiator 28*14*11MM Graphics Card Heatsink Custom Color Length Aluminum Radiator IC Heat Sink Cooler
Custom anodized compact cooler with pre-applied thermally conductive double-sided tape for power supplies, motor drives, and inverter modules.
Engineering Tactile Membrane Switches for Central American Tropical Climates
A comprehensive design specification for procurement directors, embedded hardware engineers, and systems integrators deploying control panels in high-salinity, high-humidity Caribbean environments.
1. Architectural Stratification and Material Selection for Saline-Atmosphere Operation
In industrial human-machine interfaces (HMI), standard commercial-grade membrane keyboards experience rapid dielectric breakdown, silver migration, and tactile spring fatigue when operated in humid subtropical regions such as Belize. Bordered by the Caribbean Sea and subjected to year-round relative humidity exceeding 85% with intense ambient ultraviolet irradiance, equipment operated across Belize City, San Pedro, Placencia, Belmopan, and Corozal demands an advanced multi-layered interface stack engineered against ingress and ionic erosion.
At Shenzhen Mivo Electronics Co., Ltd., our engineering methodology isolates mechanical snap action from chemical contamination through a tightly bonded 6-to-8 layer lamination matrix. The foundation rests upon premium biaxially oriented polyethylene terephthalate (PET) films (predominantly MacDermid Autotex® XE fine-grain polyester or Dupont Mylar®). Unlike inferior polycarbonate (PC) substrates that undergo micro-fissuring and yellowing when exposed to solar UV-A and UV-B spectra, Autotex® XE provides exceptional outdoor weatherability, ensuring more than 5 million actuations without surface embrittlement or graphic fading.
| Layer Component | Material Specification | Thickness (μm) | Functional Performance in Tropical Belize |
|---|---|---|---|
| Graphic Overlay | Autotex® XE Textured Polyester / Hardcoated PET | 150 - 200 | Chemical resistance against agro-fertilizers, rum distillate, salt fog; 99% UV cutoff. |
| Overlay Adhesive | 3M 467MP / 468MP 200MP High-Performance Acrylic | 50 - 130 | Resists shear slippage under 45°C ambient temperatures and heavy Caribbean monsoon humidity. |
| Dome Retainer | Optically Clear Oriented PET with Precision Vents | 75 - 100 | Securely positions tactile domes, incorporates hermetic internal anti-condensation venting channels. |
| Tactile Dome Matrix | Stainless Steel SUS301 (Gold/Nickel Plated) | 100 - 120 | Provides 250g to 450g crisp snap feedback; rated for >1,000,000 cycles without snap fatigue. |
| Circuit Layer | Electrolytic Copper FPC or Low-Ohmic Silver Traces | 35 - 125 | Passivated with graphite carbon ink bridges; prevents dendrite short-circuits under electrical bias. |
| Rear Mounting Seal | 3M 300LSE / 9472LE Extreme High-Tack Adhesive | 100 - 150 | Forms waterproof hermetic bond to stainless steel, powder-coated aluminum, or ABS enclosures. |
The mechanical actuation dynamic relies on precision-formed metal domes available in four-legged (cross), oblong, or round configurations. For Belize industrial operators—who frequently wear heavy protective rubber gloves when operating agricultural extractors, citrus juice presses, or aquaculture processing lines—a trip force (actuation force) of 350g to 450g is standard. This tactile crispness prevents accidental input while providing tactile feedback through gloved fingertips, eliminating the need for audible buzzers in noisy processing plant floors.
Belize Industrial Sectors: Field Application Scenarios
How Mivo Electronics' tactile membrane switches, custom PCBA assemblies, and sensor modules integrate into the backbone of Belize's manufacturing, extraction, and eco-infrastructure.
1. Sugar Cane Milling & Citrus Extraction
In northern Orange Walk and Corozal districts, sugar processing facilities like the Tower Hill sugar factory operate continuous bagasse crushing, clarification boilers, and centrifugal syrup extractors. Standard electromechanical switches suffer ingress from pulverized sucrose dust and washdown spray. Mivo's IP67-rated tactile membrane switches with embossed key perimeters provide an impervious surface that withstands daily pressurized washdowns with hot caustic soda solutions, eliminating sticky actuator seizure.
2. Marine Vessel & Port Navigation Consoles
Operating along the Belize Barrier Reef, water taxi fleets, commercial shrimp trawlers, and Port of Belize logistics terminals encounter relentless salt-water mist. Salt deposit crystallization creates conductive electrical paths in traditional pushbuttons. Our sealed membrane switches utilize complete perimeter gasket sealing with 3M 300LSE adhesive and integrated status LEDs with anti-glare, matte-finish overlays, safeguarding navigation panels and winch controllers against maritime salt spray corrosion (tested under ASTM B117 standards).
3. Eco-Resort Hybrid Solar Inverters & Pumping
Remote eco-tourism sanctuaries in Cayo and offshore cayes (Ambergris Caye, Caye Caulker) rely extensively on off-grid photovoltaic power generation, reverse osmosis (RO) desalination plants, and battery energy storage systems (BESS). Inverter control interfaces encounter scorching sun and tropical ambient heat. Mivo's custom membrane keypads, mated with our extruded aluminum heat sinks (30*40*5mm / 28*14*11mm), deliver continuous thermal mitigation and intuitive tactile control for pump stations and battery banks.
4. Commercial Aquaculture & Tilapia Farms
Belize's aquaculture installations in Stann Creek rely on precision aeration monitoring, paddlewheel motor timing, and chemical dosing systems. Humidity levels directly over aeration basins hover near 100%. Utilizing our ultrasonic distance sensors (UART/PWM waterproof) coupled with sealed membrane switches, equipment operators calibrate feeding timers and liquid level thresholds without risking moisture ingress into sensitive motherboard electronics.
5. Beverage Bottling & Distillation Plants
Belizean rum distilleries and brewing lines require intrinsically safe, explosion-proof front panels. High-proof alcohol vapours and hot water washdown demand inert exterior interfaces. Polyester overlay materials utilized by Mivo resist alcohol, mild acids, and sanitizers without clouding or surface disintegration, ensuring switch graphics and window cutouts for seven-segment LED displays maintain pristine clarity across decades of bottling production.
6. Telecommunications & Remote Weather Telemetry
Solar-powered remote micro-weather stations tracking tropical storm activity across the Maya Mountains require low-power, zero-maintenance HMI input. Our tactile membrane switches integrate ultra-low parasitic capacitance, high-reliability tactile domes, and EMI/RFI shielding layers (aluminum foil or printed carbon grid), preventing false triggers during electrical lightning storms and high static atmospheric conditions.
Belize Procurement Trends: Transitioning from Re-Engineered Imports to Direct Chinese OEM Partnerships
Historically, engineering managers and plant operators in Belize procured replacement control assemblies, membrane panels, and instrumentation switches via intermediary distributors located in Florida or Texas. While convenient, this supply chain topology resulted in markups exceeding 200% to 400%, along with extended project turnaround cycles when proprietary overlays needed modification.
Over the past 36 months, an accelerated shift has emerged across Central America toward direct manufacturer sourcing in Shenzhen, China. This transition is propelled by three primary catalysts:
1. Modernization of Agro-Industrial Processing: Belize’s ongoing agricultural mechanization—supported by regional Caribbean Basin development initiatives—requires upgraded PLC interfaces and custom keypad designs. Rather than relying on obsolete physical pushbuttons that accumulate dirt and moisture, factories are adopting flush-mounted tactile panels with integrated LED backlighting and capacitive hybrid touch options.
2. Logistics Optimization via Miami and Regional Air Freight: Shipments from Shenzhen to Belize no longer face convoluted routing. Utilizing established DHL, FedEx, and air freight consolidation routes via Shenzhen Bao'an International Airport through Panama (PTY) or Miami (MIA) direct to Philip S. W. Goldson International Airport (BZE), prototypes arrive in Belize within 5 to 7 business days, while volume sea cargo clears through Port of Belize or Port of Big Creek in 25 to 32 days.
3. Low Minimum Order Quantities (MOQ): Traditional switch molders historically imposed rigid minimums of 1,000 to 5,000 units—unrealistic for Belize’s specialized industrial footprint. Mivo Electronics supports agile maintenance operations and specialized machine building by offering rapid membrane switch sampling and custom prototype PCBA runs from as few as 5 to 10 pieces.
Manufacturing Authority & Corporate Competence
Shenzhen Mivo Electronics Co., Ltd. combines precision engineering, on-site verified production facilities, and an end-to-end component ecosystem to support your hardware lifecycle.
Headquartered in the global electronics manufacturing capital of Shenzhen (Guangdong, China), Shenzhen Mivo Electronics Co., Ltd. operates an onsite-verified production facility backed by more than 8 years of verified global export performance. With an average verified buyer rating of 4.7 out of 5 stars, we have established our reputation as a trusted manufacturing partner for industrial OEMs, medical device developers, and contract manufacturers worldwide.
Onsite-Verified Manufacturing Facility
Our dedicated team of 51–100 specialized technical personnel operates modern screen-printing lines, computer-controlled precision laser cutters, hydraulic embossing stations, and automated SMT placement equipment across our comprehensive Shenzhen facility. Our physical facility and legal operations have passed formal onsite verification checks.
Full-Spectrum Electronics Synergy
Unlike pure graphic printing shops, Mivo Electronics is a comprehensive electronics hardware provider. We build bare multilayer PCBs, aluminum-core circuit boards (MCPCB), flexible printed circuits (FPC), and provide complete turnkey SMT/THT PCB assembly (PCBA) alongside our tactile membrane switches, custom sensors, and heatsinks.
Rigorous Quality Assurance Protocol
Every single switch circuit and PCBA undergoes stringent electrical continuity testing, insulation resistance verification (>100MΩ at 100V DC), contact resistance screening (<1Ω per trace), and mechanical tactile actuation measurement before export packaging. Full ESD-safe vacuum packaging safeguards components during international transport.
| Verified Metric | Mivo Electronics Operational Standard | Direct Advantage for Belize Buyers |
|---|---|---|
| Verification Status | Onsite-Checked & Verified by International Inspection Agencies | Zero risk of intermediary shell entities; transparent factory pricing. |
| Prototype Capability | Turnkey PCBA from 5 Pcs; Membrane Switches from 10 Pcs | Cost-effective replacement of one-off broken factory consoles and pilot R&D. |
| Engineering Collaboration | Full DFM Review (Gerber RS-274X, CAD DXF/DWG, BOM Alignment) | Errors detected prior to tooling; eliminates costly redesign delays. |
| Component Traceability | Direct Shenzhen Market Procurement with Client-Approved Alternates | Guaranteed authentic ICs, MOSFETs, and branded raw films (3M, Autotex). |
Frequently Asked Questions: Ordering Membrane Switches & Electronics from China to Belize
Clear, direct answers regarding customs clearance, shipping lead times, file formats, environmental performance, and minimum order requirements.
How does shipping work from Shenzhen, China to Belize City, Belmopan, or San Pedro?
1. Express Air Courier (DHL / FedEx / UPS): For prototype orders (5–50 pieces) or urgent factory maintenance parts, cargo is dispatched directly from our Shenzhen facility, routing through Miami (MIA) or Panama City (PTY) to Belize City (BZE). Typical transit time is 5 to 8 business days.
2. Consolidated Ocean Freight (FCL / LCL): For bulk volume switch panels, aluminum radiators, and bare PCBs, containerized shipping routes from Shenzhen/Yantian port to the Port of Belize or Port of Big Creek. Transit time averages 25 to 32 days, offering substantial cost savings for large-scale production runs. We supply comprehensive commercial invoices, packing lists, and Certificate of Origin (C/O) documentation to facilitate Belize Customs and Excise Department clearance under standard Harmonized System (HS) codes (e.g., HS 8537.10 for electrical boards and membrane control panels).
What design files do we need to submit for a custom membrane switch quote?
- Graphic Overlay Artwork: Vector files in Adobe Illustrator (.AI), CorelDRAW (.CDR), or editable PDF format showing colors (Pantone PMS or RAL codes), text, and display window placements.
- Mechanical & Dimension Drawing: AutoCAD (.DXF or .DWG) indicating outer perimeter dimensions, cutouts, key embossing styles (rim embossed, pillow embossed, or flat), tail length, and connector pitch.
- Circuit Schematic / Pinout: Pinout connection diagram (e.g., Matrix X-Y layout or Common Ground) and desired female/male connector type (e.g., 2.54mm Berg/FCI Clincher, Harwin, or ZIF 1.0mm/0.5mm FPC tail).
- BOM (If integrated PCBA): Component list with manufacturer part numbers for turnkey backplate assemblies.
Can your membrane switches endure Belize's high heat, torrential rain, and salty ocean air?
What is your Minimum Order Quantity (MOQ) for prototypes versus production?
Can you replicate an existing, damaged membrane switch without original CAD files?
What payment terms and transaction security are supported for Belize importers?
Accelerate Your Belize Hardware Project with Shenzhen's Premier HMI Manufacturer
Whether you require custom IP67 tactile membrane switches, high-density multilayer PCBA fabrication, waterproof distance sensors, or industrial heat sinks, Mivo Electronics provides direct engineering support, fast tooling, and competitive factory pricing.