Catalog of Featured Heat Sink Radiators & Electronics
Engineered to meet Swiss-Liechtenstein micro-engineering tolerances (DIN EN 755 & DIN EN 12020), our high-performance thermal profiles and integrated sensing components support prototypes from 5 pieces through to serialized high-volume OEM manufacturing.
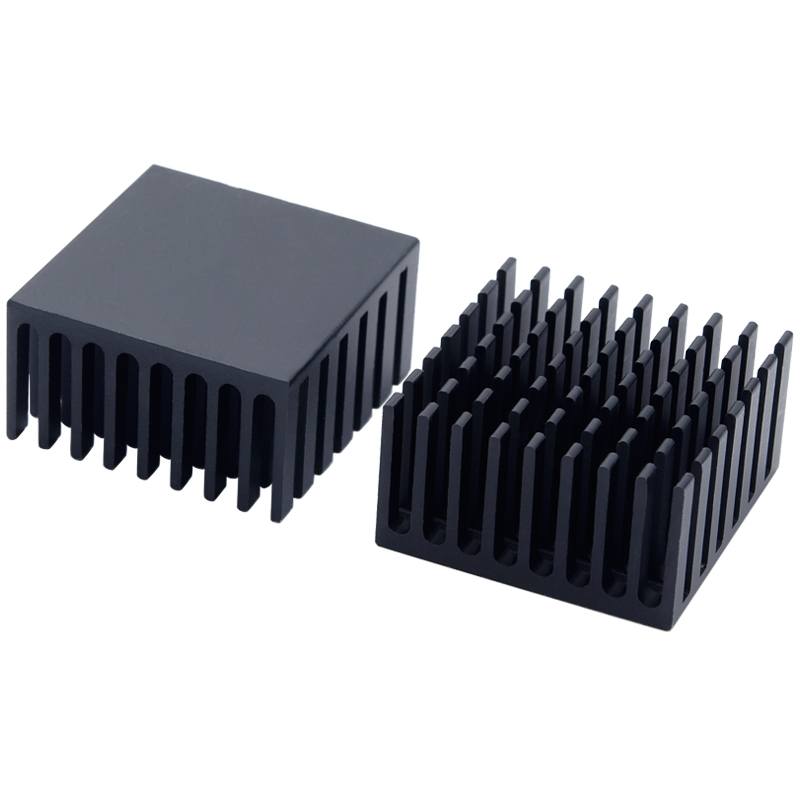
28*28*15mm Heatsink Cooling Fin Aluminum Heat Sink Radiator Cooler for Graphic Black 28X28X15mm
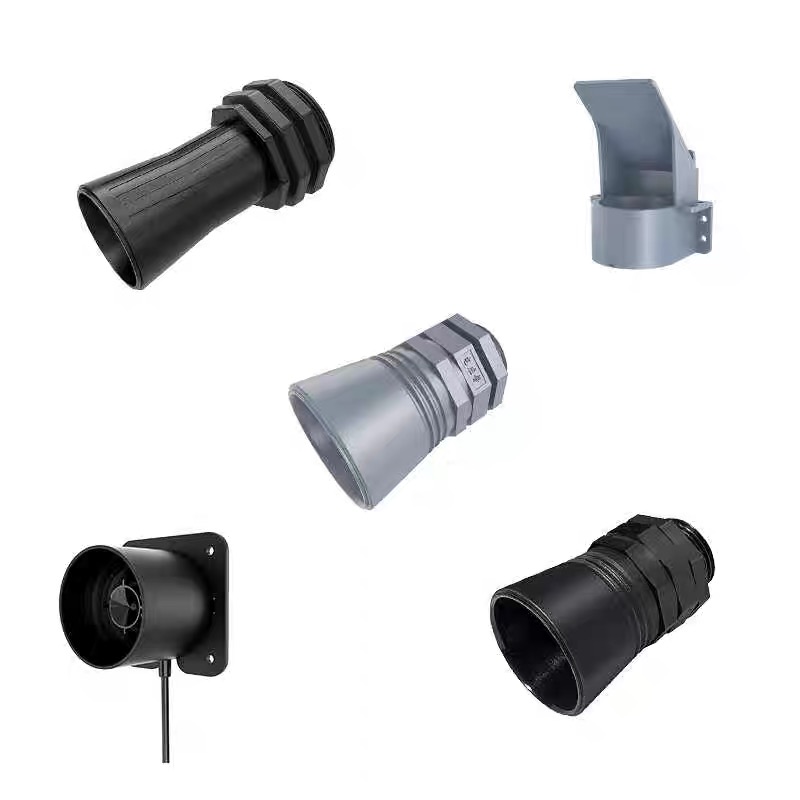
Ultrasonic Sensor Level Meter Down-well Ranging Water Level Measurement Module
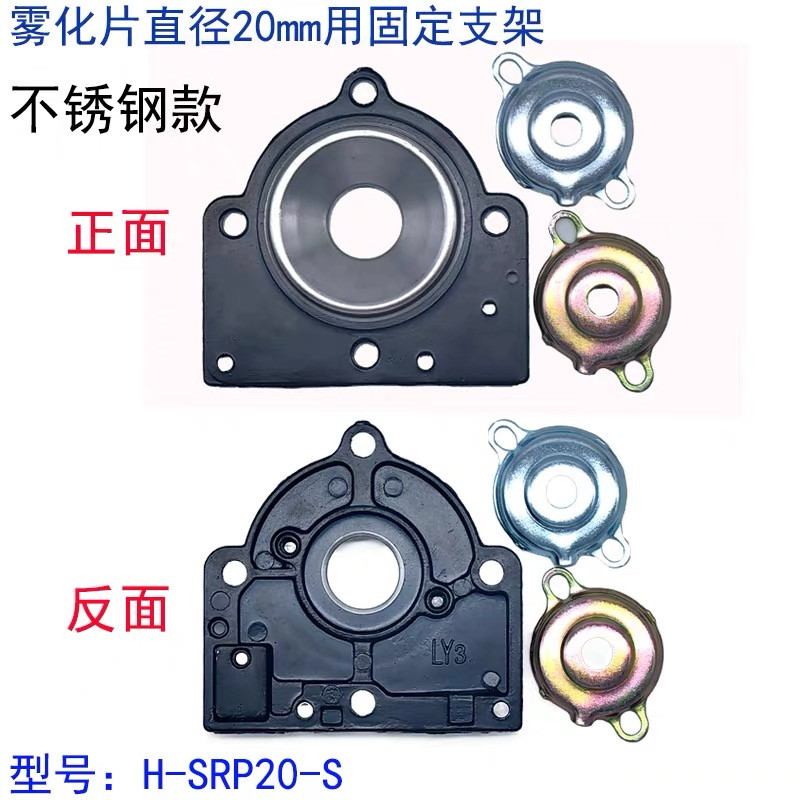
Atomizing Plate Stainless Steel Heat Sink Humidifier Accessories Atomizing Fixed Holder
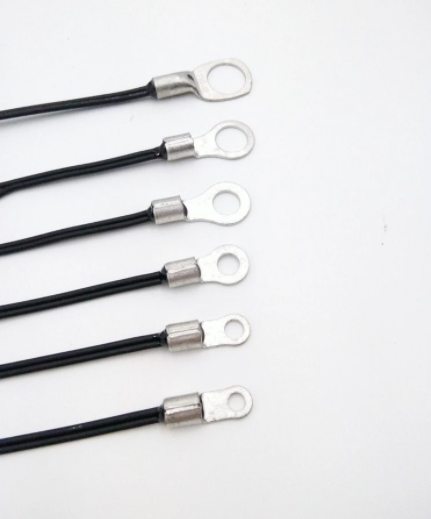
New Energy Automobile Power Battery Temperature Sensor NTC 100K Temperature Probe
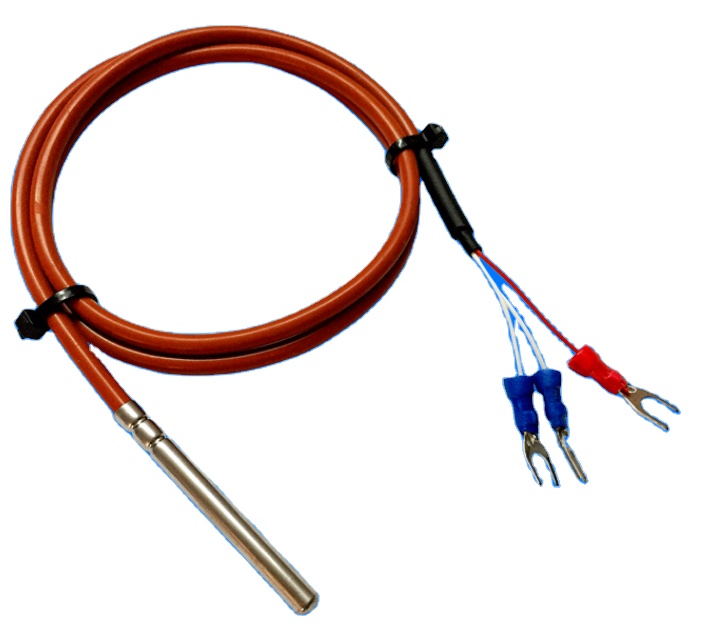
PT100 Temperature Sensor 5mm*50mm RTD Probe 3 Wire 1-5m Silicone Gel Coated
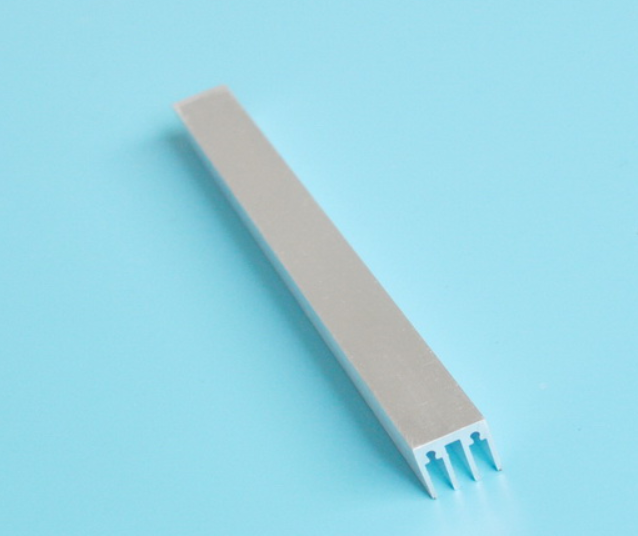
LED Comb Radiator / Light bar / Triode Radiator 16*16*100/200/300/600mm Custom Heat Sink
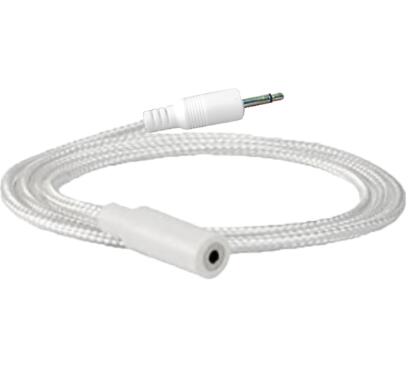
Wireless Water Leak Detection Cable Smart Home Leakage Sensing Rope
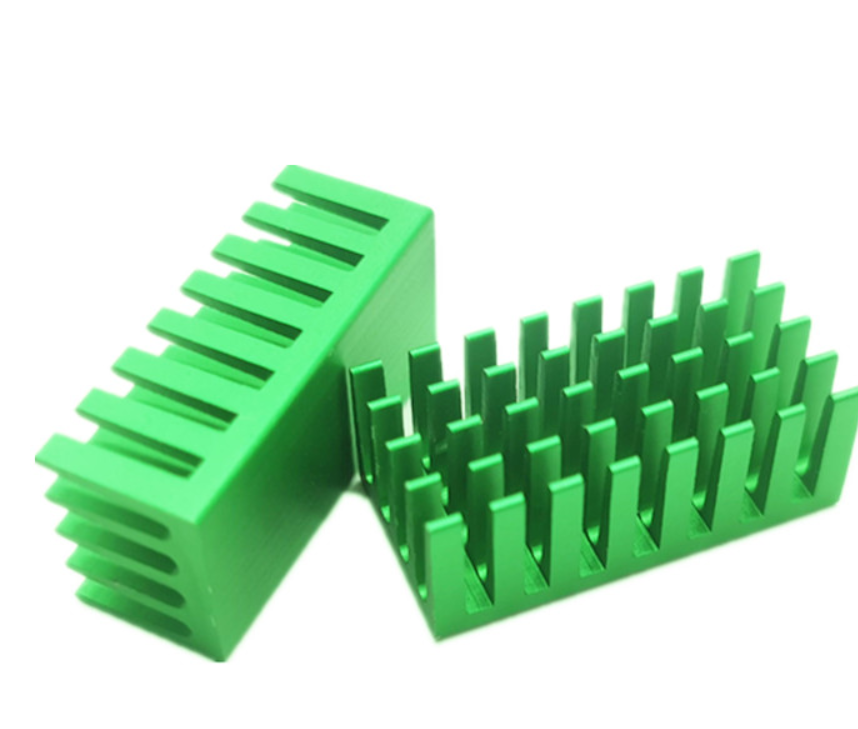
Electronic Chip Radiator 28*14*11MM Graphics Card Heatsink Custom Color Length
Metallurgical Science & Extrusion Physics for Alpine Precision Applications
Thermal management within the Rhine Valley high-tech industrial cluster—spanning Vaduz, Schaan, Balzers, and Triesen—operates under stringent dimensional stability, outgassing thresholds, and heat flux demands. As electronic devices become denser in semiconductor packaging (GaN, SiC, and high-frequency MOSFETs), the selection of aluminum alloys and the extrusion die micro-geometry directly dictate operating reliability.
Alloy Composition Matrix: AL6063-T5 vs. AL6061-T6
In thermal extrusion engineering, AL6063 remains the primary metallurgical choice for intricate fin geometry owing to its exceptional extrudability and superior thermal conductivity. Containing 0.2–0.6% Silicon and 0.45–0.9% Magnesium, AL6063 in the T5 artificial aging temper achieves a bulk thermal conductivity of 201–209 W/(m·K). This enables high fin-aspect ratios (exceeding 18:1) and thin tip structures down to 0.7 mm, optimizing the boundary layer airflow in forced convection.
Conversely, for structural radiator enclosures requiring mechanical load-bearing capacity—such as automotive chassis electronic enclosures or industrial drive inverters—AL6061-T6 is implemented. While its thermal conductivity sits slightly lower at 151–167 W/(m·K) due to higher copper (0.15–0.40%) and chromium content, it provides superior yield strength (276 MPa vs. 145 MPa for 6063-T5) and exceptional thread-tapping shear resistance for heavy DIN-rail mounting hardware.
Selecting the Optimal Heat Sink Architecture
Comprehensive benchmarking of thermal dissipation manufacturing methodologies for Liechtenstein equipment designers.
| Thermal Technology | Thermal Conductivity | Max Fin Aspect Ratio | Tooling Investment | Prototyping Lead Time | Best Suited Application in FL |
|---|---|---|---|---|---|
| Extruded Aluminum (6063-T5) | 209 W/(m·K) | Up to 24:1 | Low - Moderate | 7–10 Working Days | Mechatronics, LED arrays, Industrial Drives |
| Skived Fin Pure Aluminum | 220 W/(m·K) | Up to 35:1 | Low (No hard tooling) | 12–15 Working Days | Ultra-dense server modules, IGBT switches |
| High-Pressure Die Casting (ADC12) | 96 W/(m·K) | 6:1 | High (Steel tooling) | 30–45 Working Days | Complex 3D housings, Automotive brackets |
| Cold Forged Pin Fin (AL1070) | 236 W/(m·K) | 15:1 (Omnidirectional) | Moderate | 15–20 Working Days | Multi-directional airflow fixtures, Spot lamps |
| Bonded / Embedded Heat Pipe Fin | Effective > 1,000 W/(m·K) | Custom Assembly | Moderate to High | 20–25 Working Days | High-vacuum instrumentation, Laser diode stages |
Localized Applications Across Liechtenstein's Key Manufacturing Sectors
Liechtenstein maintains one of the world's highest ratios of industrial output per capita. Our custom extruded radiators and thermal assemblies integrate directly into the precision production ecosystems of the Principality.
Balzers High-Vacuum & Thin-Film Coating Systems
Balzers is globally recognized for PVD and thin-film coating apparatus. In deep-vacuum environments, convective cooling ceases to function. We engineer customized AL6063 thermal mounting blocks equipped with mirror-machined contact faces (Ra < 0.4 μm) to facilitate conductive heat transfer to water-cooled cold plates without dielectric fluid contamination or outgassing.
- Outgas-free high-grade chemical black anodizing
- Embedded RTD PT100 sensor pockets for vacuum telemetry
- High flatness tolerance (< 0.02 mm across 200 mm base)
E-Mobility & Powertrain Electronics in Eschen & Schaan
With major automotive steering, drivetrain, and commercial vehicle engineering suppliers operating out of Eschen and Schaan, thermal radiators must survive extreme vibrational cyclic loads (ISO 16750-3) and thermal shocks ranging from -40°C to +125°C. Our integrated assemblies pair robust aluminum radiators with custom NTC thermistors and PT100 harness assemblies for real-time thermal throttling.
- Vibration-resistant CNC cross-cut pin patterns
- Thermal interface material (TIM) pre-application
- Custom copper heat-pipe staking for localized hotspots
Medical, Dental & Lab Robotics (Schaan & Triesen)
Liechtenstein's renowned dental materials and precision medical instrumentation industries require whisper-quiet, passively cooled enclosures for dental furnace controllers, high-speed milling CAD/CAM spindles, and laboratory diagnostic robots. Natural convection comb radiators provide passive acoustic-free heat transfer.
- Silent natural convection fin profiles with chimney draft optimization
- Bio-compatible non-conductive clear anodized finishes
- Zero burr edge chamfering (DIN ISO 13715)
Liechtenstein Sourcing Trends: Decarbonization, Miniaturization, and Turnkey Integration
Thermal management procurement within the Alpine economic zone (Liechtenstein and Eastern Switzerland) has shifted dramatically over the past 24 months. Purchasing departments and lead system architects are no longer sourcing bare heat sink profiles in isolation. The modern procurement paradigm prioritizes three core vectors:
1. Unified Thermal-Sensor-PCBA Subsystem Sourcing
Engineering departments in Vaduz and Schaan are consolidating vendors to mitigate supply-chain friction. Rather than issuing purchase orders to separate extrusion plants, CNC machine shops, SMT assembly lines, and cable manufacturers, buyers increasingly demand ready-to-mount sub-assemblies. As a dual PCBA and heat sink manufacturer, Shenzhen Mivo Electronics delivers extruded radiators pre-assembled with aluminum core PCBs (MCPCB), surface-mounted power stages, pre-calibrated PT100/NTC temperature probes, and precision silicone cabling.
2. Strict Carbon Border Adjustment Mechanism (CBAM) Readiness
Due to Liechtenstein's customs union with Switzerland and its membership in the European Economic Area (EEA), industrial components imported into the country face stringent environmental reporting standards under EU CBAM and REACH/RoHS directives. Our smelting partnerships utilize certified low-carbon recycled aluminum billets processed via hydroelectric-powered electrolysis, accompanied by complete Material Safety Data Sheets (MSDS) and full material traceability certificates (EN 10204 type 3.1).
3. Accelerated Rapid Prototyping for Iterative R&D Cycles
Liechtenstein's specialized machinery developers operate under agile product lifecycles. Traditional 6-week extrusion die lead times are unacceptable during initial proof-of-concept testing. Mivo Electronics solves this by bridging the gap: we provide 5-piece low-volume rapid prototype runs machined directly from solid billet AL6063 via high-speed 5-axis CNC milling within 5 to 7 days, before cutting dedicated extrusion tooling for serial production.
End-to-End Extrusion & Manufacturing Workflow
From initial CAD/Gerber thermal simulation to final CMM coordinate validation and ESD-safe export packaging.
DFM & Thermal Simulation
Finite element thermal analysis (FEA), fin pitch optimization, and extrusion die flow modeling.
Billet Pre-heat & Extrusion
Tightly monitored 480°C–520°C billet pressing through precision tungsten carbide extrusion dies.
T5/T6 Age Hardening
Precipitation heat treatment yielding optimal Webster hardness (≥ 12 HW) and crystalline stabilization.
Precision CNC Milling
Multi-axis CNC drilling, pocketing, tapping, fly-cutting, and counterboring to ±0.01 mm tolerances.
Surface Passivation
MIL-A-8625 Type II anodizing (clear, matte black, bespoke colors) or trivalent chromate conversion (RoHS).
Optical & CMM Inspection
100% surface inspection, contact flatness verification, and optical coordinate profiling.
Why Alpine Tier-1 & Tier-2 OEMs Partner with Mivo Electronics
Combining the cost efficiency of Shenzhen's industrial supply chain with Swiss-level precision quality control.
Onsite-Verified Manufacturer
Physical production facilities in Yuanshan Street, Shenzhen verified on-site by third-party inspection agencies. Operating transparently on international export platforms for over 8 consecutive years with an average buyer review score of 4.7 / 5.0.
Turnkey Electronic Co-Design
Unlike standard aluminum foundries, we specialize in turnkey PCBA, Multilayer & Aluminum Core PCBs, membrane switches, and custom sensors. We deliver fully mounted, thermal-interfaced, and electrically validated modules ready for enclosure installation.
Extreme Prototyping Flexibility
We respect engineering development cycles. While conventional extrusion suppliers enforce minimum order quantities of 500 kg to 1 metric ton, Mivo supports custom prototypes starting from just 5 pieces with dedicated DFM engineering support.
Seamless Central European Logistics
Full familiarity with Swiss-Liechtenstein customs declarations (EFTA framework, EUR.1 origin certification assistance, DDP via Zurich Airport air-freight hubs). We ensure zero customs hold-ups at the Buchs/Schaanwald border clearance points.
Frequently Asked Questions by Liechtenstein Purchasing & Engineering Teams
Detailed technical, regulatory, and commercial answers addressing common procurement considerations.