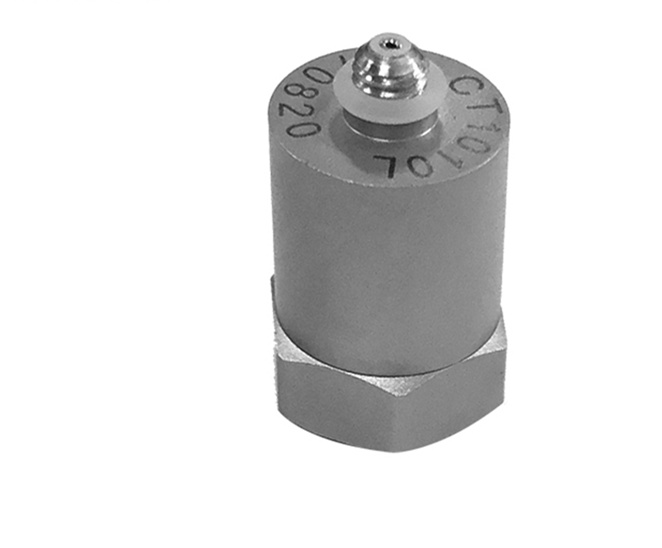
Dynamic Sensing
Each module engineered to integrate seamlessly with membrane interfaces, embedded controller boards, and rugged industrial enclosures operating throughout Bitola's core industrial sectors.
Bitola's industrial ecosystem, anchored by the Pelagonia energy corridor, precision agricultural processing, and specialized manufacturing, demands human-machine interface (HMI) controls that perform under relentless mechanical, chemical, and environmental stress.
We manufacture tactile membrane switch assemblies utilizing premium biaxially-oriented polyethylene terephthalate (PET) and optical-grade polycarbonate (PC). The micro-layered construction combines subsurface reverse screen printing, conductive silver flex circuits with carbon overcoats, and industrial acrylic pressure-sensitive adhesives (3M 467MP / 468MP) to eliminate circuit migration and delamination caused by high ambient thermal swings.
Mining dust from the Suvodol and Brod-Gneotino open-cast basins, combined with acidic washdown cycles in local dairy and food processing plants, rapidly degrades unprotected controls. Our peripheral gasket-seal geometry integrates continuous perimeter adhesive barriers and breather-channel venting that equalization systems block liquid moisture, caustic alkalis, and fine particulate penetration completely.
Incorporating gold-plated and nickel-plated stainless steel metal snap domes (ranging from 8mm to 20mm in diameter, with actuation forces calibrated between 220g and 450g), our switches provide crisp mechanical feedback with an actuation life exceeding 1,000,000 cycles. We optimize tactile snap ratios to ensure workers wearing heavy industrial safety gloves receive unambiguous tactile confirmation upon switch closure.
From large-scale power generation at REK Bitola to high-speed bottling lines and advanced automotive components in the Bitola Industrial Zone (TIDZ Bitola), membrane HMIs serve as the primary operational frontline.
High-vibration mining machinery, lignite excavators, and conveyor systems at REK Bitola operate in environments laden with sulfurous ash, coal particulate, and extreme mechanical shock. Our customized membrane keypads feature solid-state shielding, UV-stabilized Autotex polyester surfaces, and integrated LED indicator arrays designed to withstand heavy vibration profiles when paired with IEPE accelerometer monitoring systems.
Pelagonia is the agricultural powerhouse of North Macedonia, home to massive dairy processors (such as Bimilk) and beverage bottling operations. Production floor consoles undergo daily high-pressure chemical washdowns with chlorine, peracetic acid, and hot steam. Our IP67-rated seamless membrane overlays prevent fluid ingress, eliminate microbial harboring crevices, and resist chemical degradation over years of service.
International automotive wire harness and electronics assembly plants located in the Technological Industrial Development Zone (TIDZ Bitola - Zabeni) require rigorous test benches, testing jigs, and custom operator interface panels. We supply low-profile, ESD-shielded membrane switches that connect via standard 2.54mm or 1.00mm pitch FPC connectors directly into digital PCBA testing modules.
Bitola's historical light manufacturing and textile workshops are continuously modernizing legacy machinery with smart PLCs and automated controllers. Replacing obsolete mechanical pushbuttons with custom multi-key membrane panels allows factory managers to modernize their equipment front panels, integrate clear operational schematics, and prevent lint and dust accumulation inside sensitive electrical enclosures.
A comparative overview designed by our engineering department to assist Bitola procurement officers and electrical design engineers in selecting the optimal overlay material and circuit construction.
| Substrate / Parameter | Autotex Biaxially-Oriented PET | Optical Polycarbonate (Lexan PC) | Polyimide Flex PCB (Copper FPC) | Silver Conductive Screened PET |
|---|---|---|---|---|
| Primary Mechanical Role | Graphic Overlay & Top Layer | Overlay & Display Windows | High-Density Switch Circuit Core | Cost-Effective Flexible Circuit |
| Actuation Flex Life | > 5,000,000 continuous cycles | ~ 100,000 cycles (embossed) | > 10,000,000 cycles | > 1,000,000 cycles |
| Chemical & Solvent Resistance | Exceptional (Alcohols, Acetone, Acids) | Moderate (Prone to aromatic attacks) | Excellent (Withstands Soldering flux) | Protected beneath adhesive layers |
| Operating Temperature | -40°C to +85°C | -30°C to +105°C | -40°C to +125°C | -20°C to +70°C |
| Tactile Dome Compatibility | Stainless Steel Dome, Polydome | Flat Non-Tactile, Polydome | Surface SMT Domes & Solderable LEDs | Placed under polyester spacer pocket |
| Best Suited Application | Pelagonia Food/Dairy CIP lines | Indoor Instrumentation & Medical | Critical Energy & Automotive TIDZ | General Industrial Machinery Panels |
Understanding the structural shifts in North Macedonia’s industrial core helps domestic manufacturers implement forward-compatible user interface solutions.
While tactile metal domes remain standard for machinery where operators require positive physical feedback through gloves, Bitola's modern food packaging, beverage processing, and pharmaceutical lines are transitioning to solid-state capacitive membrane panels. Capacitive touch surfaces eliminate mechanical moving parts entirely, enabling flat glass or thick acrylic front layers that can be disinfected effortlessly without wear.
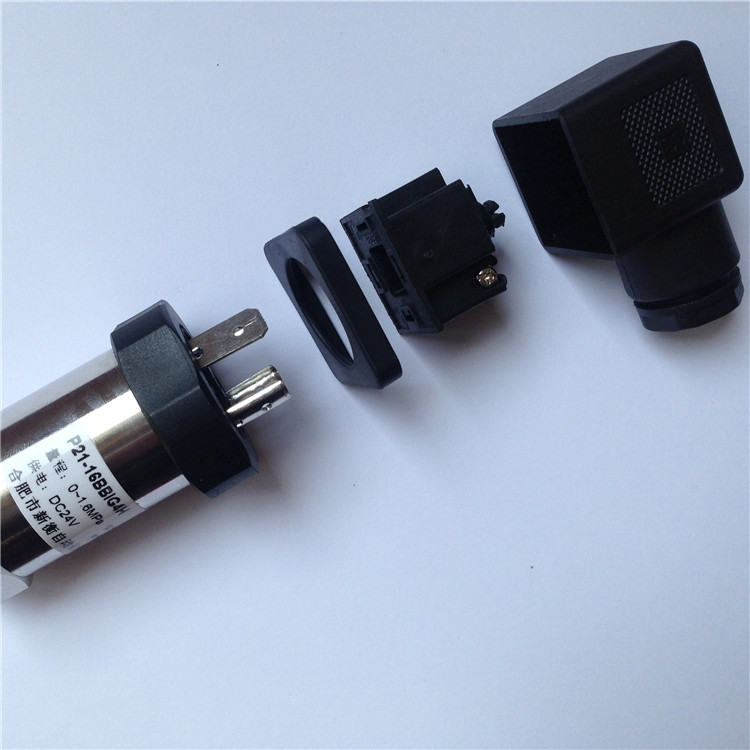
Human-machine interfaces are no longer isolated switch arrays. In modern Pelagonia facilities, membrane switch assemblies are directly integrated with peripheral sensors: temperature RTD probes (such as PT100 elements), liquid level sensors, vibration monitors, and humidity transmitters. By embedding the switch panel with a turnkey PCBA carrier board, our solutions act as compact telemetry and control endpoints communicating over RS485 or CAN bus.
With North Macedonia committing to decarbonization and the progressive decommissioning and transition of lignite units at REK Bitola toward solar PV, gas, and hybrid generation, industrial facilities are aggressively refurbishing energy management infrastructure. This transformation requires custom switchboards, compact secondary sub-station consoles, and specialized operator panels manufactured to precise mechanical tolerances.
Direct-from-factory electronic manufacturing services with verified onsite facilities in Shenzhen, China. We bridge European industrial design standards with China's rapid electronic component ecosystem.
Unlike trading middlemen, Shenzhen Mivo Electronics integrates bare PCB fabrication, multi-layer circuit printing, electronic component sourcing, SMT assembly, and custom membrane switch manufacturing under one roof. Bitola clients eliminate the overhead of managing separate overlay printers, board houses, and wiring harness shops, ensuring perfect electrical continuity from switch tail to mainboard socket.
Our factory premises have passed comprehensive third-party onsite verification by Alibaba.com and international auditing bodies. Prior to tooling and production, our senior engineering staff performs rigorous Design for Manufacturability (DFM) reviews on every drawing, checking trace clearance, dome actuation spacing, tail bend radiuses, and environmental seal paths to prevent field failures.
We manage fast, reliable express air freight (via DHL, FedEx, and UPS) directly into Skopje International Airport (SKP) and Thessaloniki Airport (SKG), ensuring expedited customs transit directly to your facilities in Bitola. For ongoing volume production, we offer multimodal sea and rail cargo options providing competitive landed costs with full export documentation, certificates of origin, and RoHS/CE compliance declarations.
Direct answers addressing technical files, lead times, minimum orders, and customization for engineering and purchasing departments.