Wireless Water Leak Detection Cable Smart Home Leakage Sensing Rope
Distributed fluid presence sensing line optimized for industrial plant floors, server rooms, and building automation nodes across Salzburg.
Custom engineered hardware assemblies matching rigorous European industrial standards. From custom membrane keyboards to integrated thermal and sensing components, explore our verified OEM solutions.
Distributed fluid presence sensing line optimized for industrial plant floors, server rooms, and building automation nodes across Salzburg.
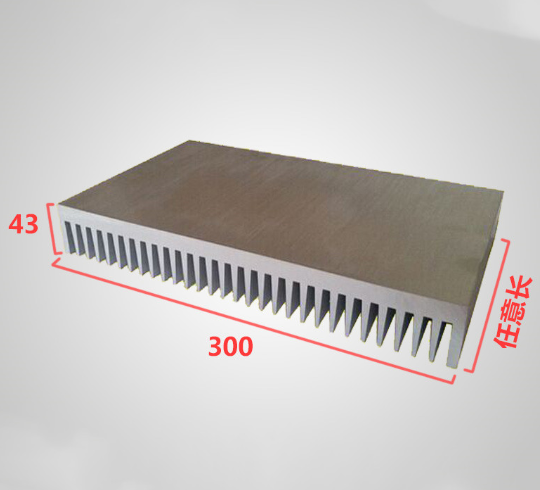
Heavy-duty extruded aluminum profiles engineered for high-wattage power amplifiers, EV charging points, and motor drive controllers.
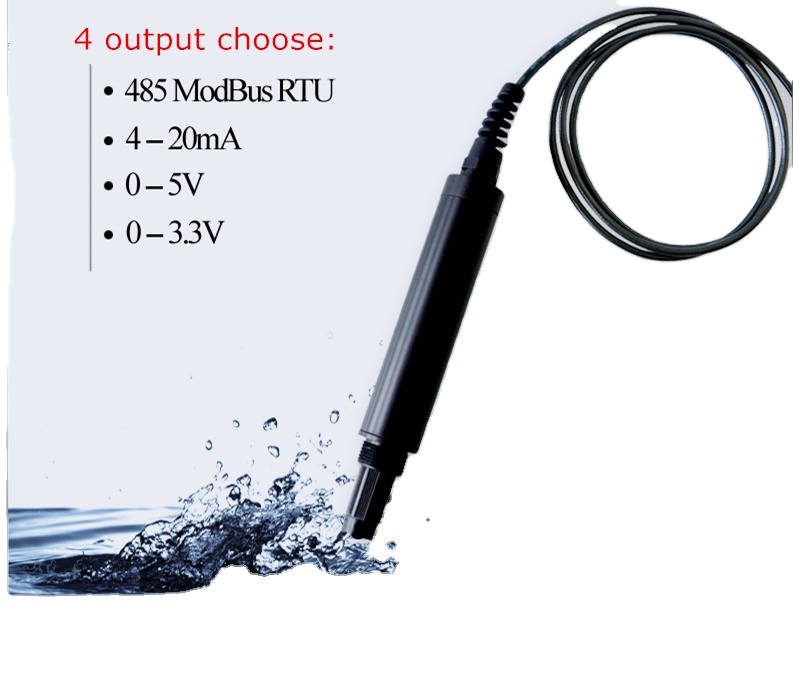
High-stability electrochemical probe delivering digital RS485 Modbus/4-20mA telemetry for Austrian beverage, wastewater, and bioreactor lines.
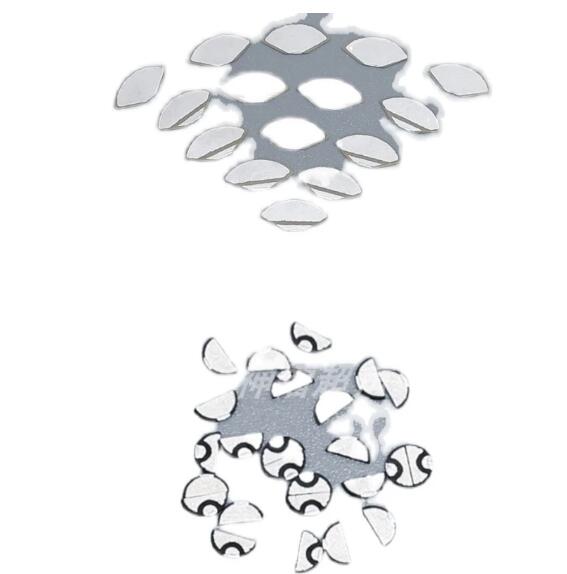
Multi-frequency sector ceramics designed for non-destructive testing (NDT), ultrasonic flow meters, and precision acoustic waveguides.
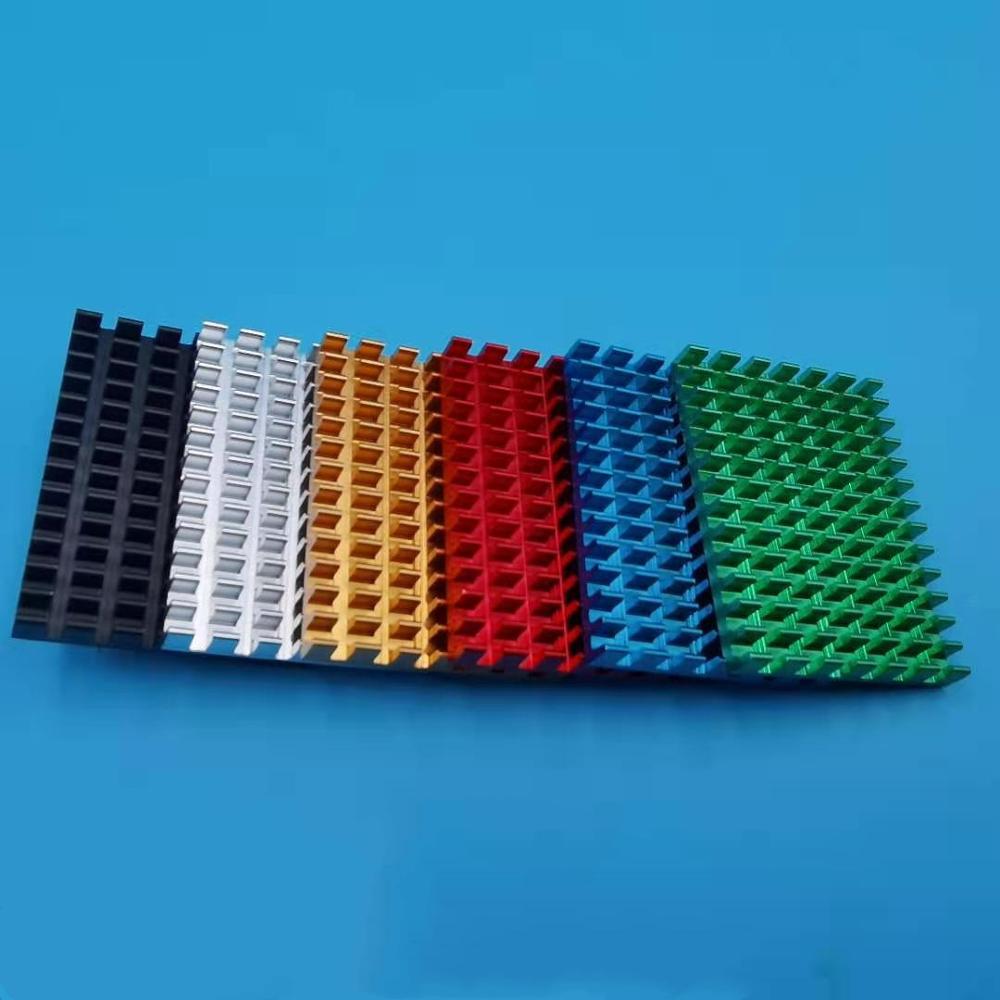
Compact low-profile thermal sinks tailored for dense multi-layer PCB boards, router microchips, and compact industrial gateways.
Robust down-well ranging module with IP68 transducer encapsulation, perfect for municipal drainage systems and industrial water reserves.
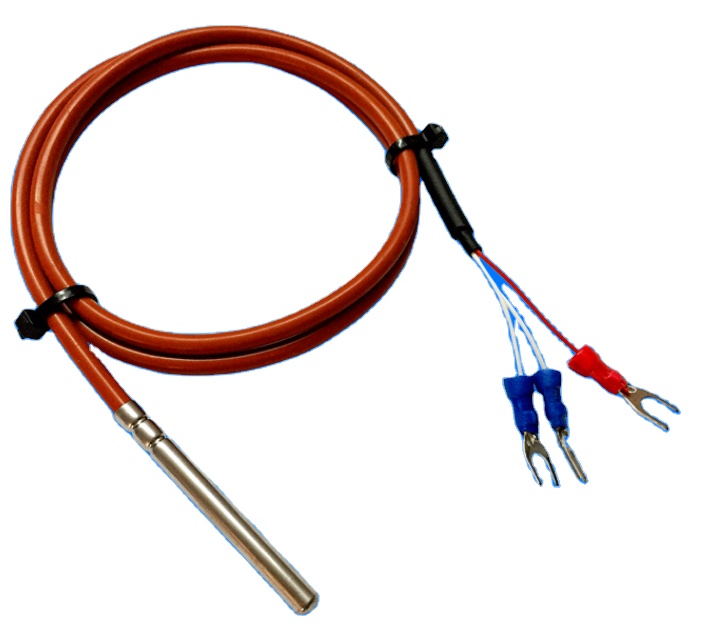
Class A platinum resistor probe with silicone insulation, built for broad thermal tolerance (-50°C to +200°C) and corrosive washdowns.
Sintered stainless-steel filter housing safeguarding digital I2C humidity telemetry in high-condensation, cold-storage, and cleanroom air.
Within the industrialized regions of Salzburg, Hallein, Seekirchen, and St. Johann, modern machinery manufacturers, medical technology pioneers, and automation developers demand Human-Machine Interfaces (HMI) that marry aesthetic cleanliness with relentless physical durability. The membrane switch keyboard has fundamentally transitioned from an austere tactile layer into a sophisticated electromechanical nexus. Today's OEM panels integrate embedded surface-mount LEDs, capacitive slider interfaces, full ESD/RFI shield layers, optical bonding, and rigid-flex PCB backings capable of surviving millions of mechanical actuations.
As export partners to European original equipment manufacturers, we observe that the primary vulnerability in alpine industrial setups is rapid thermal cycling and moisture condensate ingestion. Facilities that alternate between freezing alpine atmospheric intake and aggressive indoor radiant heat produce localized internal condensation. Conventional sub-assemblies experience circuit silver migration and eventual short circuits. Our custom OEM membrane keyboards solve this via high-adhesion 3M 200MP/300LSE adhesive sandwich gasketing, micro-vented GORE membranes that equalize barometric variations without compromising IP67 ingress protection, and carbon-overprinted silver traces that stop dendritic degradation completely.
Selecting the exact material stack-up is pivotal for equipment operational lifespan in Austrian food processing, clinical diagnostics, and robotic automation environments:
| Switch Parameter | Standard Polyester Screen-Printed | Copper Flex Circuit (FPC) Backed | Rigid FR-4 PCB Core Integrated |
|---|---|---|---|
| Actuation Life Cycle | 1,000,000 to 2,000,000 Cycles | 3,000,000 to 5,000,000 Cycles | 5,000,000+ Cycles (Tactile Metal Dome) |
| Operating Temperature | -20°C to +65°C | -40°C to +85°C (Alpine Spec) | -40°C to +105°C (High Power Modules) |
| Tactile Feedback Type | Polydome (Embossed PET) or Steel Dome | Nickel/Gold-plated Stainless Dome | Precision Tact Switches or Metal Dome Array |
| Component Integration | SMD LEDs with conductive epoxy | Direct SMT Soldering (Resistors, ICs, Micro-controllers) | Full Turnkey SMT & THT (High-density PCBA) |
| Chemical Resistance | Autotex Steel/Fine Finish (Alcohols, Oils) | Full Gasket Seal + Chemical Resilient Overlay | Hermetic Enclosure Mount + O-Ring Gasketing |
From alpine lift monitoring systems to pharmaceutical grade packaging, membrane switches perform in critical environmental conditions throughout the federal state of Salzburg.
Salzburg’s ski infrastructure and mountain rescue networks require weather-sealed operator panels resistant to sub-zero freezing, blinding UV rays, and gloved operational pressure.
Salzburg’s biomedical research and hospital laboratory equipment manufacturers require sterile, anti-microbial interfaces capable of handling regular aggressive chemical wipe-downs.
In the Alpine forest and wood manufacturing clusters surrounding Salzburg, wood dust, vibration, and hydraulic spray destroy unshielded tactile panels rapidly.
Salzburg's strategic location along the Austrian-German border makes it a critical logistical and technical node connecting Bavarian engineering powerhouses with Central European industry. In this competitive landscape, three macro developments are driving procurement choices for custom OEM membrane switch keyboards:
1. Convergence of Capacitive Touch and Physical Tactile Domes: Modern Austrian equipment manufacturers no longer treat capacitive touchscreens and membrane keyboards as mutually exclusive. Modern designs incorporate hybrid layouts: high-resolution capacitive touch displays for complex navigation coupled with embossed, physical tactile membrane switches for emergency stops, axis calibration, and safety-critical overrides. This layout prevents catastrophic mis-clicks caused by water drops or grease splashes on pure touchscreens.
2. Full Turnkey Sub-Assembly Migration (Box-Build Readiness): Purchasing departments in Salzburg are actively reducing vendor complexity. Rather than buying a bare membrane switch, sourcing a distinct PCB from another supplier, and contracting local assembly houses, OEMs now insist on receiving integrated, tested units. Our facility produces the bare PCB, sources the components, prints the overlay, assembles the metal domes, mounts the connectors, and delivers ready-to-mount modules directly to your production line.
3. Compliance with Strict Eco-Design and RoHS/REACH Audits: In accordance with strict Austrian Federal Environmental Regulations and European Union directives, our export switches undergo strict testing for halogen-free adhesives, RoHS-compliant solder pastes, and non-toxic UV inks, preventing customs delays and regulatory fines during CE machine certification.
Based in the global hardware epicentre with verified onsite credentials, we blend Shenzhen speed with strict European quality control protocols.
Our manufacturing plant, testing chambers, and assembly lines have passed rigorous onsite inspections by Alibaba.com and third-party inspection firms. We operate as an authentic manufacturer, not a broker.
Eliminate multi-vendor finger-pointing. We manage everything under one roof: multi-layer PCB manufacturing, SMT stencil laser cutting, component procurement through Shenzhen channels, and precise membrane switch layering.
We respect Austrian prototyping cycles. PCBA and custom sensor prototypes start from 5 pieces, while membrane switches start from small verification runs, scaling to hundreds of thousands of production units with consistent yields.
Every engineering package is subjected to strict Design For Manufacturability (DFM) reviews: checking circuit trace clearances, contact resistance limits, tail bend radii, and dome actuation clearances before hard tooling begins.
Maintaining a 4.7/5 customer rating over 8+ years of global exporting. We provide bilingual technical support, transparent delivery schedules via DHL/FedEx/air freight, and seamless customs paperwork for direct EU importation.
Beyond keypads, integrate matching thermal management (aluminum heat sinks), waterproof PT100 temperature probes, or ultrasonic sensors into your end machine enclosure in a single, consolidated shipment.
Straightforward technical and commercial answers addressing tooling costs, tactile life-cycles, import customs, and engineering documentation.
We require the vector graphic overlay artwork (Adobe Illustrator, CorelDRAW, or PDF with Pantone/RAL color codes), dimensional mechanical drawings showing key positions and tail outlet points (AutoCAD DWG/DXF or STEP), and a schematic or wiring matrix pinning table for the connector output.
We implement a continuous outer perimeter gasket using hydrophobic 3M 300LSE/VHB adhesive laminates that completely enclose the active conductive silver traces. For atmospheric pressure equilibrium without water intake, we incorporate breathable, liquid-impermeable ePTFE membrane vent patches.
Yes. Many Austrian clients choose our complete box-build or sub-assembly service. We can bond the membrane keyboard directly to an anodized aluminum or plastic injection-molded chassis plate, connect the flexible tail to our SMT-assembled PCBA, and test the entire unit prior to export packing.
Rapid prototype samples with laser-cut tooling generally ship within 7 to 10 working days following DFM approval. Mass production runs with hard-tooled die sets take approximately 15 to 20 working days. Express air courier transit to Salzburg Airport (SZG) or Vienna (VIE) typically takes 3 to 5 business days.
We calibrate our production line using electronic force-displacement testers. Standard stainless steel dome actuation forces range from 250g to 450g depending on whether your application requires light finger operation or positive high-force gloved feedback. Every batch includes a detailed Cpk report for tactile consistency.
We provide full commercial invoices with precise HS code classifications (typically 8537.10 or 8538.90 for switch panels and electronic control bases), certificates of origin, and packing lists. Shipments can be arranged under standard Incoterms including EXW, FOB, CIF, or DAP directly to your manufacturing site in Salzburg.
Connect directly with our engineering and procurement team. Send us your CAD drawings, overlay schematics, or Gerber packages to receive a comprehensive DFM manufacturability evaluation and competitive OEM quotation within 24 hours.