Factory-Direct Sensor & Thermal Radiator Solutions
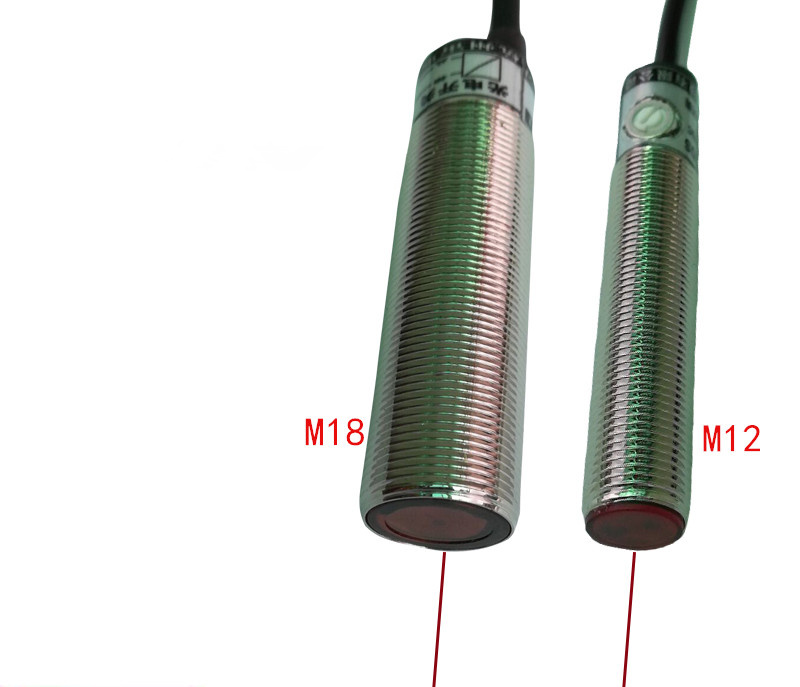
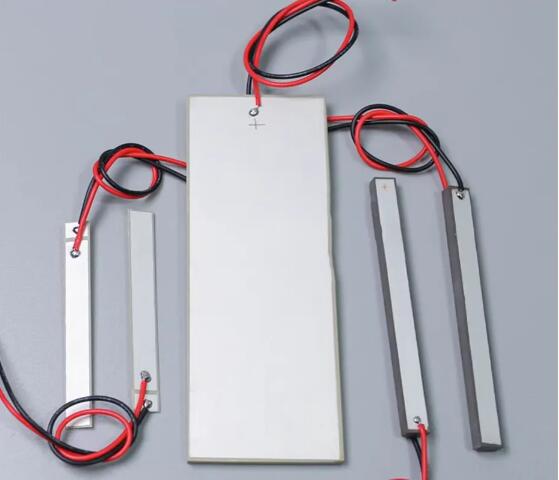
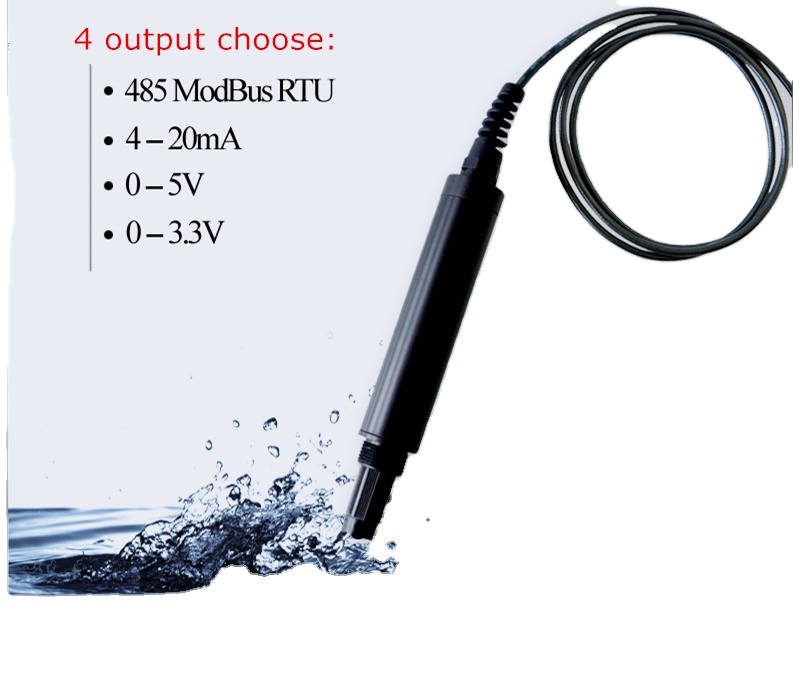
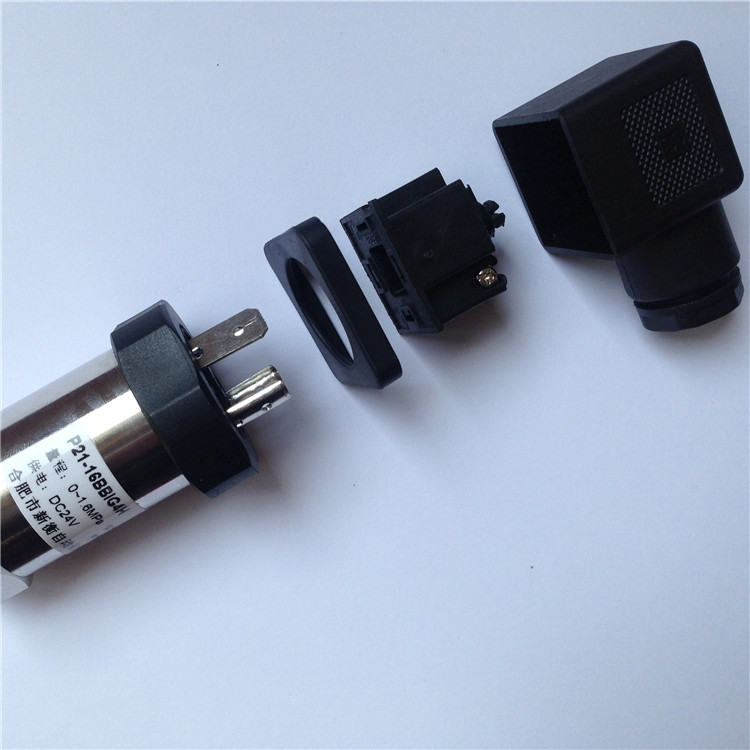
Alongside custom embossed membrane switches, Shenzhen Mivo Electronics delivers precision optoelectronics, liquid level sensors, heat sinks, and industrial transducers integrated directly into finished Caribbean control consoles.
Engineering Whitepaper: Tactile Embossed Membrane Keypads for Kingston’s Harsh Operating Environments
In modern electronic equipment manufacturing, the Human-Machine Interface (HMI) serves as the primary operational touchpoint. For procurement engineers, system integrators, and plant operations managers operating throughout Kingston, Jamaica, standard commercial grade input panels consistently fall short. Kingston’s unique environmental profile—characterized by sustained equatorial UV radiation index (UVI > 11), high ambient relative humidity fluctuating between 70% and 92%, and intense airborne saline concentration originating from Kingston Harbour and the Caribbean Sea—demands an engineered, industrial-grade embossed membrane switch architecture.
Shenzhen Mivo Electronics Co., Ltd. bridges the gap between precision high-reliability manufacturing and international export logistics. Operating from our onsite-inspected Shenzhen production facility, we engineer multilayered custom membrane switches utilizing heat-stabilized polyester substrates (Autotype MacDermid Autotex XE and Autoflex), proprietary selective embossing methodologies, and hermetically sealed perimeter gasketing. By preventing delamination, silver migration, and contact oxidation, our switches ensure continuous operational reliability across port container terminals, agro-industrial rum distillers, food processing lines, and critical municipal infrastructure across the Greater Kingston Metropolitan Area.
Substrate Selection & Precision Embossing Topographies
The graphic overlay constitutes both the aesthetic interface and the primary defense shield of any membrane switch. Where standard commercial keypads employ low-cost Polycarbonate (PC) that yellows, embrittles, and cracks under tropical sunlight within 12 to 18 months, our export assemblies specified for Kingston mandate biaxially-oriented polyethylene terephthalate (PET) with advanced outdoor UV stabilizers. Polyester films demonstrate superior flex life exceeding 5 million actuations, extreme chemical inertness against petrochemical fuels and industrial clean-in-place (CIP) sanitizers, and remarkable tensile yield strength.
Rim (Perimeter) Embossing
Elevates an acute ridge around the button perimeter (0.3mm to 0.5mm profile), guiding operator finger placement in low-light environments without accidental activation.
Pillow (Plateau) Embossing
Uniformly elevates the entire key surface area. Ideal for wide graphic legends, emergency shut-off pads, and operators wearing heavy chemical or thermal gloves.
Polydome Forming
Thermoformed polyester tactile bubbles engineered directly into the polyester overlay layer. Delivers positive snap-action feedback without discrete metallic internal domes.
Braille & Tactile Guides
Precision hydro-formed tactile dots conforming to international accessibility standards, facilitating sightless operational telemetry in public terminals.
Mechanical Stack-Up Architecture & Environmental Gasketing
A resilient membrane switch operates as a precision multi-tier mechanical laminate. Delamination or internal moisture condensation is the most frequent mode of failure in tropical island climates. To guarantee hermetic sealing, Shenzhen Mivo Electronics implements a multi-layer composite bonded with acrylic transfer tapes from 3M (such as 3M 467MP for smooth backplates and 3M 468MP or 3M 300LSE for low-surface-energy powder-coated enclosures).
| Layer Index | Material Specification | Thickness Range | Functional Contribution |
|---|---|---|---|
| 1. Graphic Overlay | Autotex XE UV-Resistant Textured PET | 0.13mm – 0.20mm (5 – 7 mils) | UV barrier, chemical shielding, sub-surface graphical screen printing. |
| 2. Overlay Adhesive | 3M 467MP High-Performance Acrylic | 0.05mm (2 mils) | Permanent, non-degassing bonding between overlay and dome retainer. |
| 3. Tactile Spring Layer | Stainless Steel Domes (Nickel / Gold Plated) | 0.08mm – 0.12mm (Tripod/4-leg) | Snap-action tactile sensation, 280g–450g actuation force, 1M+ cycles. |
| 4. Spacer Layer | Die-Cut Heat-Stabilized Mylar (PET) | 0.10mm – 0.18mm (4 – 7 mils) | Establishes dome travel channel, isolates conductors, vents dome cavities. |
| 5. Circuit Layer | Screen-Printed Conductive Silver / Carbon Ink | 0.10mm – 0.125mm (4 – 5 mils) | Low-impedance conductive traces (<100Ω), silver migration barrier ink. |
| 6. Rear Mount Adhesive | 3M 468MP or 3M 300LSE High-Tack Adhesive | 0.13mm (5 mils) | Guarantees permanent adherence to aluminum, steel, or molded plastic chassis. |
Localized Application Scenarios Across Kingston's Industrial Landscape
Kingston acts as the economic engine and commercial shipping epicenter of the English-speaking Caribbean. Industrial applications within this economic district face distinct mechanical stressors. Our custom manufactured membrane switches are intentionally tailored to integrate seamlessly across four vital Kingston sectors:
Port Automation & Maritime
Kingston Wharves and the Kingston Container Terminal represent pivotal transshipment hubs. Crane operator consoles, container gantry pendants, and deck-mounted marine pump controllers operate under constant marine salt spray and tropical torrential rains.
- NEMA 4X / IP67 perimeter sealing gaskets
- Anti-glare textured surfaces under blinding sun
- Stainless steel domes resisting saline corrosion
Agro-Industrial & Distilling
Jamaica's world-renowned rum distilleries, food packing houses, and sugar processing refineries along the Industrial Terrace corridor mandate switches capable of enduring rigorous high-pressure clean-in-place (CIP) protocols.
- Resistance to ethanol, caustic sodas, and steam
- Seamless flat-surface design preventing bacteria traps
- Embossed rim overlays for glove-wearing operators
Medical & Life Sciences
Medical testing equipment, hospital diagnostic devices, and clinical analytical machinery stationed at the University Hospital of the West Indies require hygienic, non-porous HMI panels that can withstand regular sterilization.
- Medical-grade antimicrobial polyester films
- Impervious to isopropyl alcohol and bleach washes
- Tactile confirmation preventing operational error
Future Trends: Evolution of HMI Solutions in the Caribbean Industrial Sector
The Caribbean Basin is currently undergoing a massive digital infrastructure modernization. Kingston's utility operators, manufacturing plants, and logistics firms are pivoting from antiquated electro-mechanical pushbuttons to high-density smart control assemblies. In our engineering design centers, we observe three definitive technical evolutions requested by Caribbean procurement leads:
1. Backlit Capacitive Hybrid Interfaces: Traditional membrane switches are evolving into integrated capacitive touch solutions where discrete mechanical tactile domes coexist with proximity touch zones. By utilizing micro-diffused light guide films (LGF) or side-firing LEDs mounted directly to thin flexible printed circuits (FPC), interface backlighting is achieved with ultra-low power consumption, perfect for solar-powered remote installations across rural Jamaican telemetry substations.
2. Silver Migration Mitigation via Carbon Overprinting: When high-voltage potential differences interact with pervasive relative humidity, electrochemical migration (silver whiskers) historically plagued cheap membrane circuits. Shenzhen Mivo Electronics implements proprietary carbon ink overprinting over silver conductor tracks, creating a permanent electrochemical barrier that guarantees uninterrupted electrical isolation and prevents short circuits even in unconditioned coastal control enclosures.
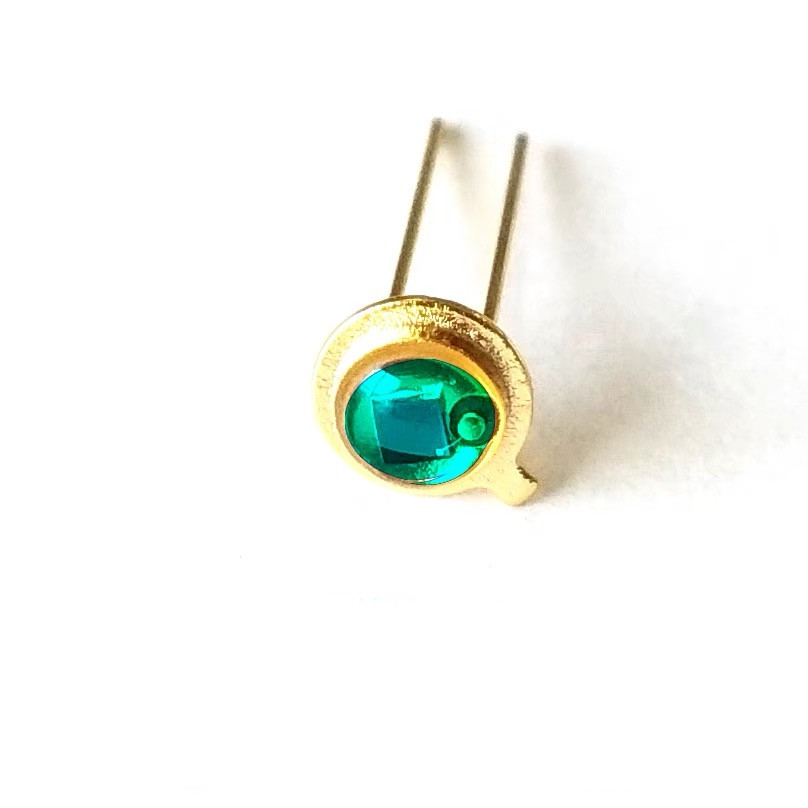
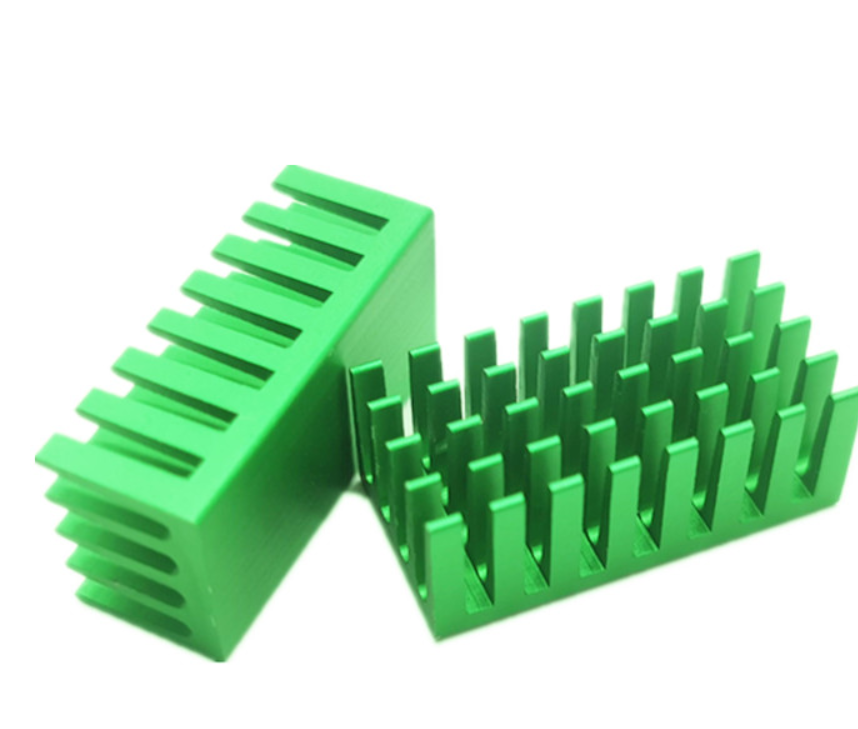
3. Turnkey Integration with Sensors and Rigid PCB Modules: Modern OEMs in Kingston no longer order membrane switch panels in isolation. Instead, they seek fully assembled, factory-tested control units. As shown in our featured product showcase, we provide unified sub-assemblies integrating custom tactile overlays with rigid FR4 backer boards, onboard microcontrollers, optoelectronic photodiode modules, ultrasonic tank-level monitors, and custom aluminum heat sinks for an out-of-the-box drop-in installation.
Kingston Procurement FAQ: Sourcing Membrane Switches from Factory Direct
What is the minimum order quantity (MOQ) for custom embossed membrane switches exported to Kingston?
How does Shenzhen Mivo Electronics protect membrane switches from Kingston’s high heat, humidity, and salt fog?
What file formats and design documentation are needed to receive a formal quotation and DFM report?
What are the typical international air freight transit times and customs procedures for delivery to Jamaica?
Can you integrate backlighting, display windows, and surface-mount LEDs within the membrane switch?
How do you verify the quality and tactile performance of each switch before export shipment?
Shenzhen Mivo Electronics Co., Ltd.
As an onsite-verified electronics manufacturer operating in the heart of Shenzhen's industrial cluster, Shenzhen Mivo Electronics delivers an all-inclusive manufacturing ecosystem. We eliminate intermediate supplier margins by combining precision membrane switch production, bare PCB fabrication, turnkey SMT/through-hole assembly (PCBA), and custom sensor engineering under one rigorous quality management structure.
Whether you require 5-piece bespoke HMI prototypes for a maritime automation upgrade in Kingston Harbour or 50,000 high-durability keypad overlays for export-ready appliances, our team of 51–100 manufacturing professionals delivers predictable quality, transparent engineering documentation, and proactive DFM support.
- Business License StatusOnsite Verified Manufacturer
- Production LocationYuanshan Street, Shenzhen, China
- Year Established2016 (Verified Continuous Trading)
- Workforce Scale51 – 100 Skilled Personnel
- Quality VerificationAlibaba Verified Supplier (8 Yrs)
- Customer Rating4.7 / 5.0 Star Verified Score
- Core CapabilitiesMembrane Switches, PCB, PCBA, Sensors
- Target Export PortNorman Manley Airport / Kingston Port
Request an Immediate Engineering Review & Quotation
Send us your vector graphics, enclosure drawings, or electrical schematics. Our engineering team reviews all Caribbean inquiries within 12 hours with complete DFM feedback.
Contact Us