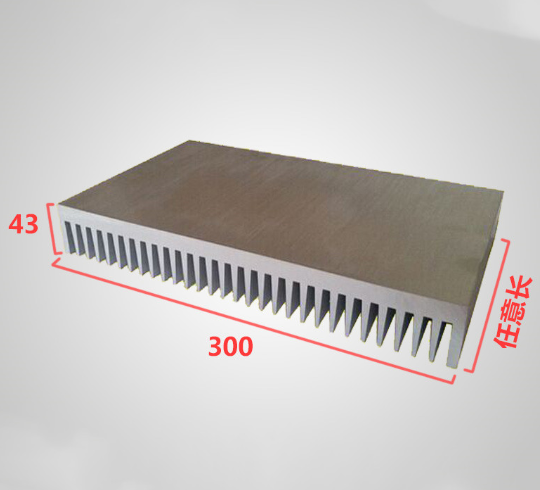
High-Power Aluminum Radiator Heat Sink Cooling Plate (300*43mm)
Designed for heavy thermal dispersion in ruggedized HMI backplanes and industrial control boxes.
Engineered to operate seamlessly alongside custom LED membrane switches, PCBA controllers, and telemetry modules in harsh industrial environments.
Designed for heavy thermal dispersion in ruggedized HMI backplanes and industrial control boxes.
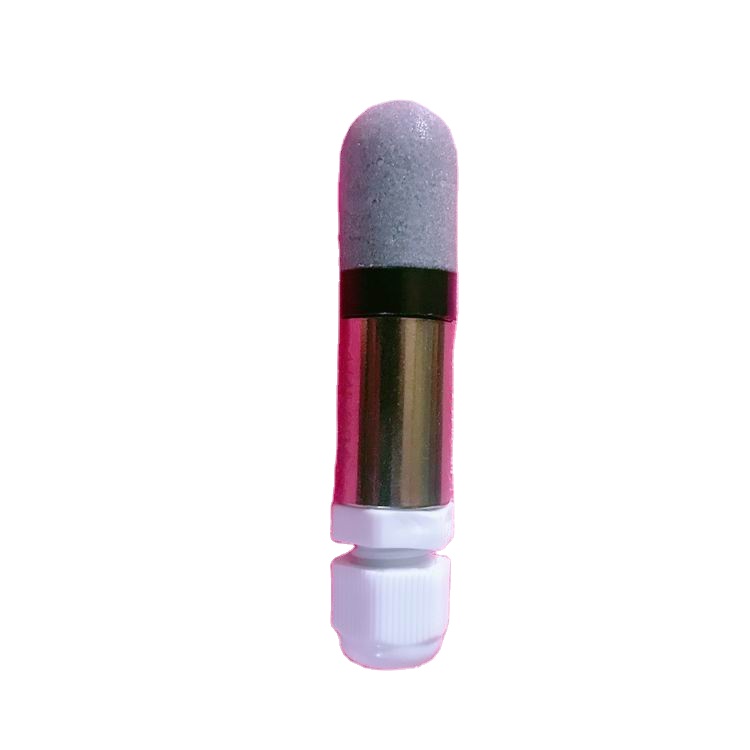
Protective housing cover ensuring IP67/NEMA 4X weatherproofing in demanding environmental monitors.
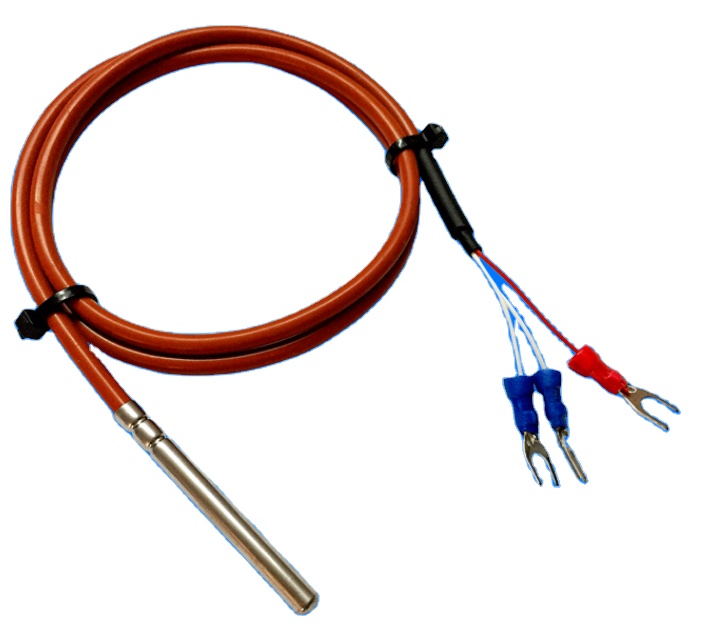
Waterproof and oil-proof sensor probe providing precision feedback across sub-zero Calgary installations.
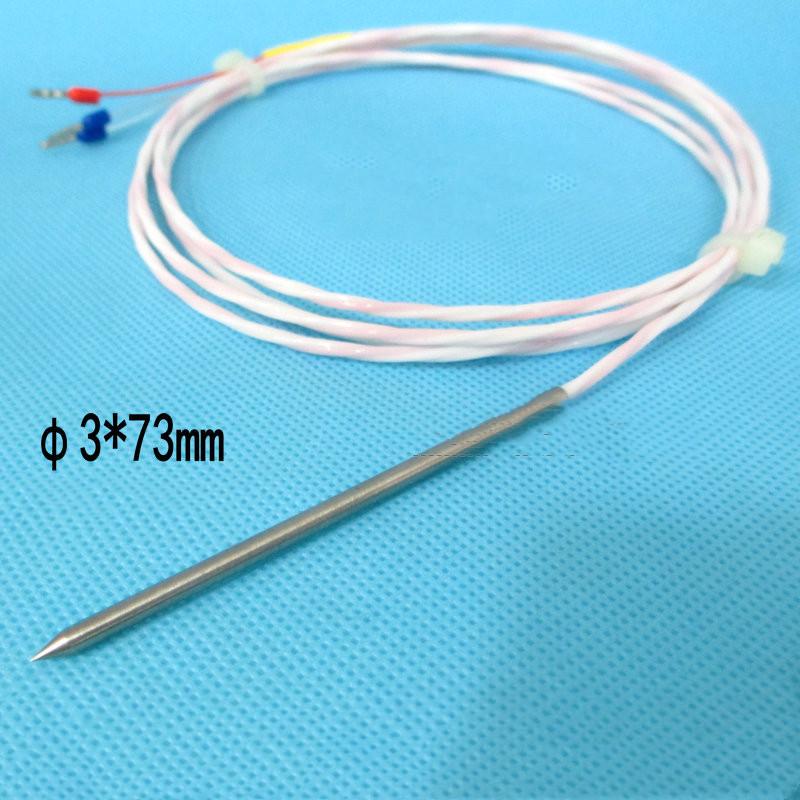
Ultra-accurate penetration temperature sensors engineered for automated chemical and agricultural testing.
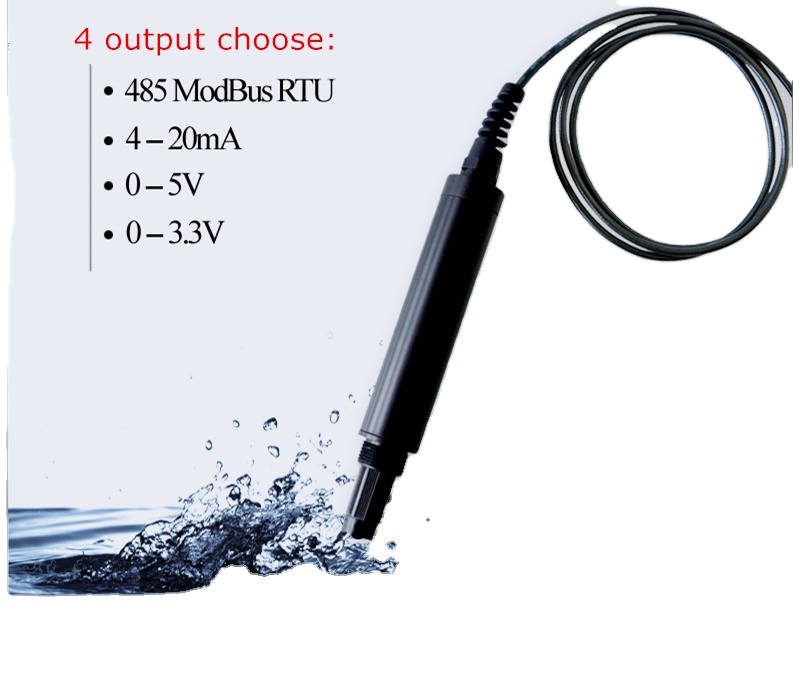
Industrial telemetry electrode designed for water treatment plant monitoring and municipal pipeline integration.
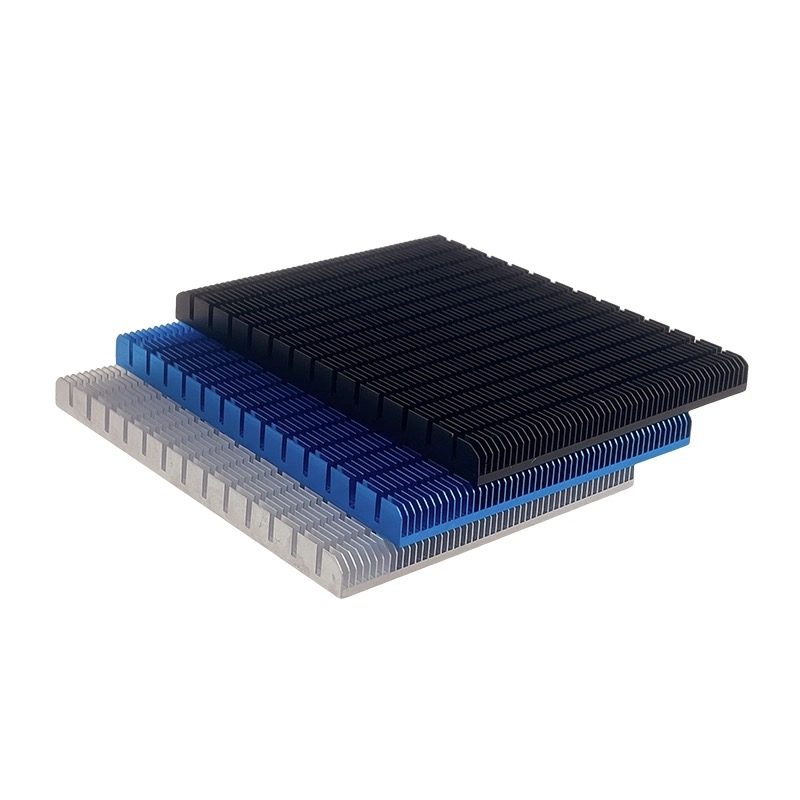
Pre-applied thermally conductive tape for rapid passive dissipation in micro-controllers and display drivers.
Distributed fluid sensing system for clean rooms, server racks, and automated smart building infrastructure.
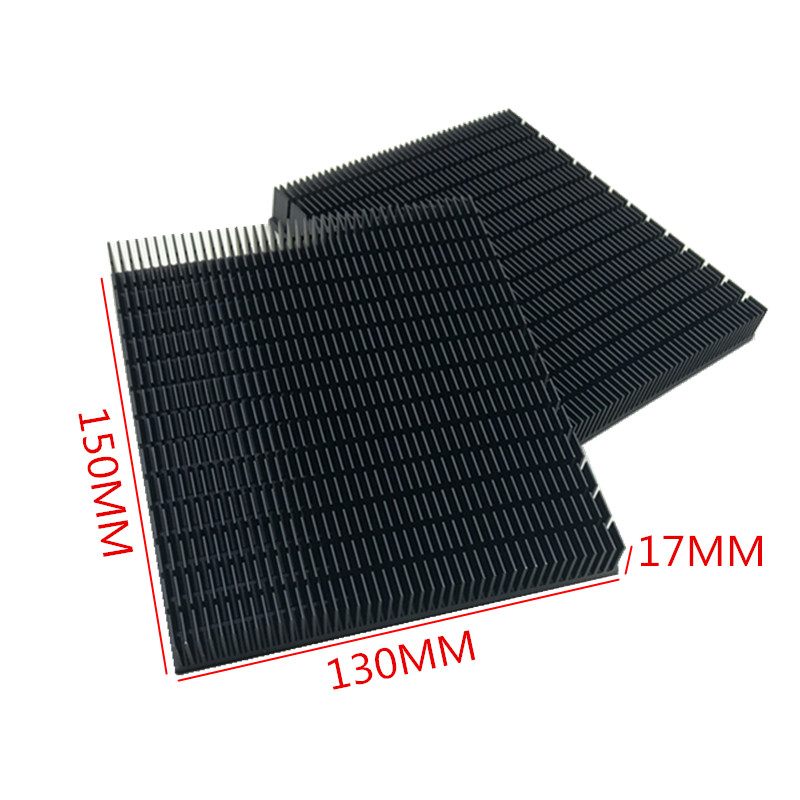
High surface area grooved profile engineered for continuous high-load industrial power supply cooling.
Bridging surface-mount optoelectronics with robust multilayer polyester and polycarbonate interfaces.
In Calgary, Alberta, ambient temperatures routinely cycle from -40°C during winter cold snaps to above +35°C during summer industrial operations. Standard commercial membrane switches degrade rapidly under these conditions due to disparate coefficients of thermal expansion (CTE) between the flexible polyester substrate (PET), printed silver conductive traces, anisotropic conductive adhesive (ACA), and surface-mounted chip LEDs. Shenzhen Mivo Electronics implements stress-relief trace routing geometry combined with flexible conductive silver polymer paste enriched with low-temperature plasticizers. This ensures that as the overlay flexes or contracts under thermal shock, trace micro-cracking and SMT LED delamination are completely engineered out.
Integrated micro-patterned polymethyl methacrylate (PMMA) or silicone diffusion conduits redistribute directional SMT LED light evenly across keys, eliminating hotspots and chromatic aberration while reducing total power consumption on remote Calgary battery installations.
Utilizing high-cohesion 3M 200MP / 300LSE modified acrylic adhesive systems paired with continuous gasket boundaries. This prevents volatile hydro-carbon ingress, airborne dust, and high-pressure steam washdown water penetration.
Incorporated solid or grid-patterned carbon, copper, or aluminum layers shunted to system ground. Our assemblies resist ESD arcs up to 15kV, safeguarding sensitive internal PCBA logic boards against winter static discharge common in dry Alberta interior facilities.
| Architecture Feature | Standard Commercial Membrane Switch | Mivo Industrial Ruggedized LED Switch | Calgary Engineering Benefit |
|---|---|---|---|
| Operating Temperature | -10°C to +50°C | -45°C to +85°C | Zero failure during winter freeze-thaw cycles |
| Overlay Graphic Substrate | Standard Monolithic PVC / Untreated PET | Autotype MacDermid F200/V200 Hardcoat PET | Resistant to diesel, glycol, hydraulic fluids & UV radiation |
| LED Encapsulation | Rigid Epoxies prone to brittle fractures | Elastomeric UV-Curable Flexible Resins | Absorbs physical impact and localized tactile deflection |
| Tactile Actuation Feedback | Flat switch / Unsealed domes (<500k cycles) | Nickel-Plated Stainless Steel Domes (>1,000,000 cycles) | Crisp tactile snap through thick winter work gloves |
| Thermal Dissipation Interconnect | Direct mount to thin polyimide | Thermal Via Linking to Aluminum Core (MCPCB) | Extends MTBF of high-lumen status indicators |
Custom-engineered human-machine interfaces deployed across oil & gas, automated ag-tech, transportation, and green utility grids.
Calgary is Canada's energy nerve center. Our LED membrane switches are fitted onto explosion-proof enclosures, Class I Div 2 flow meters, and remote SCADA controllers operating unattended in the Western Canadian Sedimentary Basin.
Deployed in automated grain elevators, seed sorting systems, and fertilizer application units throughout Southern Alberta. Resistant to continuous chemical washdowns, fertilizer salt dust, and high mechanical shock.
Equipping heavy machinery, emergency vehicles, and light rail auxiliary electronics with back-lit, anti-glare control panels readable under intense direct sunlight and operable by operators wearing thick winter insulated gloves.
Supporting solar farm inverters, wind turbine base controllers, and hydrogen pipeline monitoring nodes around Brooks and Southern Alberta with ultra-low draw LED indication arrays built for 20-year lifespans.
The transformation of Alberta from traditional extraction to intelligent digital energy automation requires a paradigm shift in human-machine interface design.
Calgary's hardware engineers are increasingly shifting away from standalone mechanical switches toward smart membrane interfaces that integrate seamlessly with peripheral micro-controllers, digital temperature/humidity transmitters (such as Mivo's SHT30/31 arrays), and Modbus RS485 sensors. Membrane switches now serve as integrated dashboard nodes capable of indicating multi-colored status alerts via RGB surface-mount LEDs while housing shielded flex tails that link directly into custom multi-layer PCBA carrier boards.
Industrial machinery deployed across Alberta must satisfy strict regulatory compliance under CSA C22.2 No. 0, UL 50E environmental ratings, and CE electrostatic discharge standards. By conducting extensive DFM reviews and pairing certified flame-retardant substrates (UL94-V0) with halogen-free conductive adhesive systems, Mivo Electronics enables Calgary OEMs to accelerate their Canadian and global certification pipelines without costly board-level redesigns.
Combining onsite-verified manufacturing capabilities with direct, transparent supply chains for engineering teams in Canada.
Premises inspected and verified by third-party testing agencies and Alibaba.com auditors. Our factory runs 51–100 specialized professionals delivering ISO-grade build standards from PCB design through final membrane integration.
Accelerate your iterative hardware R&D. While other manufacturers enforce 1,000-unit minimums, Mivo supports Calgary startups and pilot engineering runs with PCBA and switch prototypes starting from just 5 pieces.
Eliminate multi-vendor friction. We fabricate bare boards, source hard-to-find components across Shenzhen's premier distributor market, mount SMT/THT parts, assemble custom PT100 sensors, and manufacture finished membrane overlays under one roof.
Clear, direct answers regarding logistics, thermal tolerances, file handoffs, and engineering modifications.