8+
Years Global Exporting
4.7 / 5
Verified Buyer Rating
5 Pcs
Low Prototyping MOQ
100%
Electrical & DFM Tested
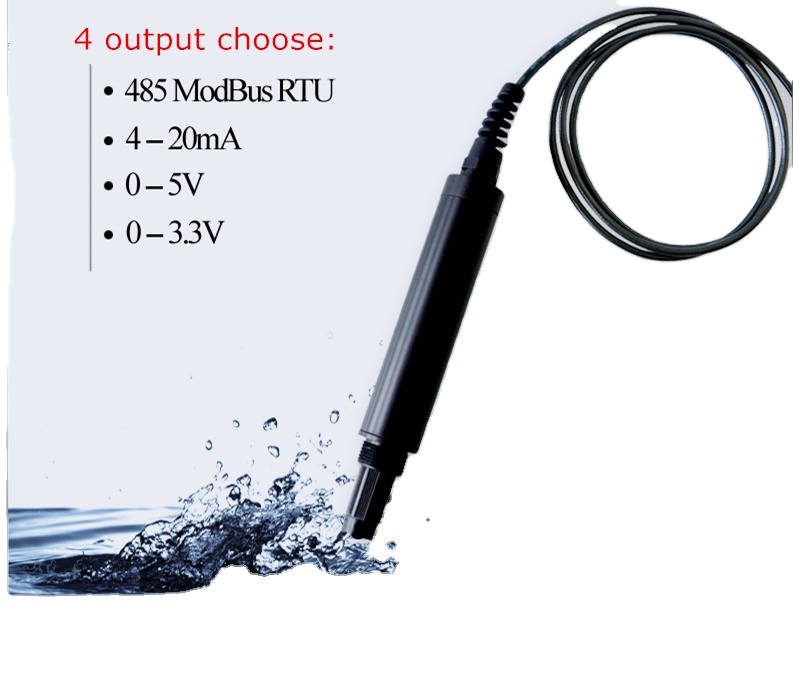
Integrated Hardware Portfolio
Specialized Sensing, Control & Interface Solutions
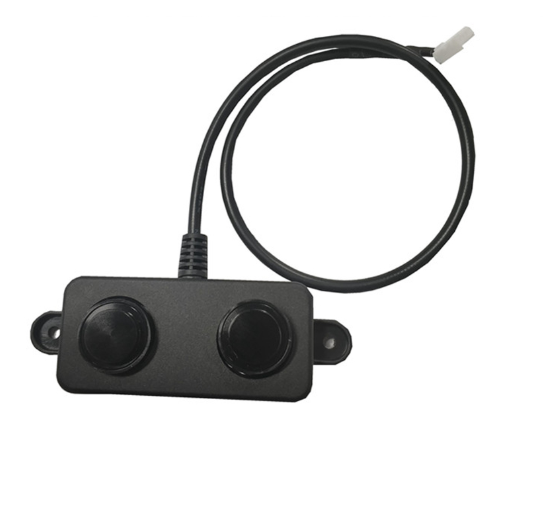
Engineered to operate seamlessly alongside our custom membrane switch panels and industrial control systems in tough environments.
Engineering Whitepaper: Designing Resilient Membrane Switches for All Saints
The parish of All Saints and its wider regional industrial sphere present unique environmental challenges for electrical controls and user interfaces. Unlike typical air-conditioned cleanrooms, human-machine interfaces (HMIs) deployed here encounter tropical atmospheric exposure, salt spray corrosiveness, seasonal humidity spikes, and heavy mechanical cycling. Finding a dependable membrane keypad supplier & suppliers for the All Saints market requires assessing engineering credentials beyond simple graphic printing.
Modern industrial membrane keypads manufactured by Shenzhen Mivo Electronics Co., Ltd. are constructed with multi-tier barrier laminations. We utilize chemically inert biaxially-oriented polyethylene terephthalate (PET) and polycarbonate (PC) graphic overlays, printed using automotive-grade ultraviolet (UV) curable inks that prevent yellowing, delamination, and embrittlement from severe sun and ambient heat. To maintain tactile feedback in high-throughput operations, our membrane switches use gold- or nickel-plated stainless steel snap domes rated up to 1,000,000 actuations, isolated by custom gasket sealers that achieve up to IP67 sealing against liquid ingress.
| Substrate / Metric | Standard Polyester (Autotex PET) | Polycarbonate (Lexan PC) | Mivo Harsh-Spec Layering |
|---|---|---|---|
| Chemical Resistance | High (Hydrocarbons, Alcohols) | Moderate (Sensitive to Ketones) | Exceptional (Fluoropolymer Barrier) |
| Flexural Endurance | >5,000,000 Switch Cycles | >100,000 Switch Cycles | Custom Annealed Silver Trace Lines |
| Operating Temperatures | -40°C to +85°C | -30°C to +105°C | -45°C to +110°C (Silicone Backed) |
| Ingress Rating Capability | IP65 Standard | IP65 Standard | Hermetic IP67/NEMA 4X Edge Seal |
Targeted Deployment
Localized Application Scenarios in All Saints
Real-world integration workflows across municipal utilities, light manufacturing, and marine-proximate facilities.
Desalination & Fluid Treatment
Water facilities rely on human-machine interfaces that handle chlorine, chemical vapors, and moisture. Our sealed membrane switches pair with DOS-600 Dissolved Oxygen sensors and Modbus controllers to ensure long-term, spark-free parameter setting.
Marine & Port Infrastructure
Material handling cranes, marine engine rooms, and winch consoles face non-stop exposure to marine salt spray. Solid-state keypad overlays prevent electrolytic corrosion across copper traces via carbon-overprinted silver interconnect pathways.
Commercial Cold-Chain & HVAC
Food storage and cooling equipment demand fast response across steep thermal differentials. Silicone-bonded and PET assemblies prevent condensation buildup behind window cutouts while preserving tactile switch feel.
Solar Inverters & Microgrids
With utility operators turning to renewable microgrids, switchgear requires UV-stabilized interface films that survive years of intense solar radiation without fading, cracking, or losing tactile dome snap.
Access Terminals & Automation
Commercial compounds require cleanable, vandal-resistant keypads. Our sub-surface graphics printing ensures legends, icons, and company branding remain intact under constant cleaning and rough sanitization.
Sanitary Medical Equipment
Clinics and field stations require seamless control panels with zero crevices where bacteria or dirt can settle, resisting harsh chemical wipe-downs from bleach, isopropyl alcohol, and quaternary disinfectants.
Market Evolution
Emerging Interface & Control Trends in All Saints
How localized electronics procurement is shifting from standalone mechanical parts to unified subsystem assemblies.
1. Convergence into Rigid-Flex PCBA + Keypad Units: Engineering teams in All Saints are cutting down on field assembly errors by purchasing fully integrated assemblies. Rather than buying loose membrane tails and mating them to separate display boards, buyers increasingly specify complete sub-assemblies: membrane panels bonded directly to FR-4 or aluminum PCB backplates, populated with SMT indicators, microcontrollers, and terminal blocks. Mivo Electronics supports this with turnkey SMT assembly lines in Shenzhen, delivering plug-and-play modules ready for final enclosure mounting.
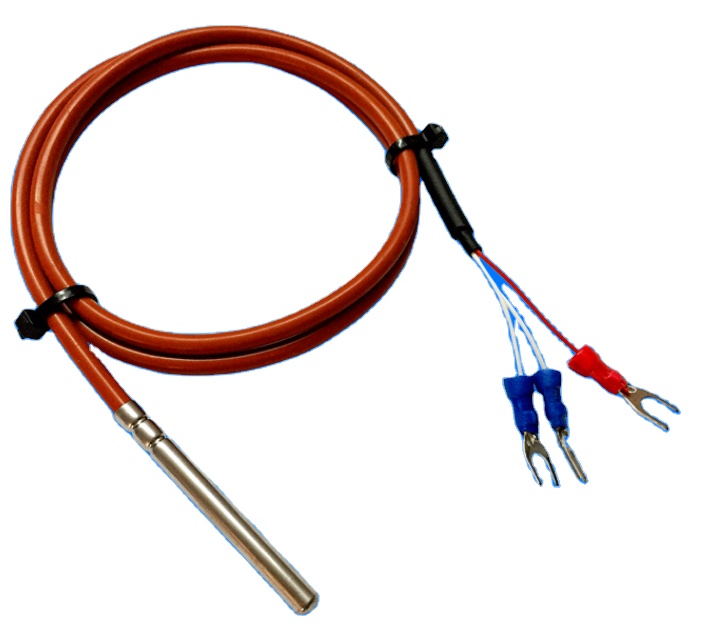
2. Smart Sensor Interfacing (IoT-Driven Telemetry): Simple on/off toggle inputs are giving way to intelligent digital dialogs. Modern field control boxes combine tactile keys with onboard real-time sensor readouts, pulling data from RTD temperature sensors, SHT30 humidity modules, or digital dissolved oxygen probes. Keypad supplier selection now hinges on the vendor's ability to verify end-to-end signal integrity and handle mixed-signal electronic design.
3. Resilience Against High Heat and Salt-Air Aging: Industrial operations cannot afford frequent switch replacements caused by trace oxidization. High silver content inks, backed with carbon-conductive masks and nickel/copper barrier plating, have become the standard build requirement for the coastal and tropical operating profiles found across All Saints.
Factory Verifiable Strengths
Why Partner With Shenzhen Mivo Electronics?
Direct factory engagement, audited quality standards, and deep component supply chain integration.
Onsite-Verified Facility
Shenzhen Mivo Electronics has been verified onsite by third-party inspection firms and global B2B platforms, confirming operational authenticity, legal licensing, and direct production lines.
Rapid Turnkey Prototyping
Eliminate multiple suppliers. We handle bare PCB fabrication, component sourcing, SMT assembly, and custom overlay printing under one roof, starting from just 5 prototype units.
Strict BOM Integrity & Testing
Every membrane switch panel, connector socket, and integrated circuit undergoes 100% trace continuity tests, switch loop resistance verification, and functional validation before dispatch.
Buyer Knowledge Base
Frequently Asked Questions for All Saints Buyers
Practical procurement insights covering environmental protection, ordering terms, and international logistics.
How do your membrane keypads withstand the humid and saline environment of All Saints?
We use premium Autotex PET film bases, high-tack 3M acrylic adhesives (such as 3M 467MP/468MP), and seal all graphic perimeter borders to IP65 or IP67 standards. Conductive silver tracks are overprinted with protective dielectric coatings to stop moisture ingress and dendritic silver migration.
What are your minimum order quantities (MOQ) for custom keypad and PCBA projects?
For prototype PCBA and custom turnkey membrane keypads, our minimum order quantity starts from just 5 pieces. Sensor listings typically start from 10 pieces, while catalog component sourcing begins between 100 to 2,000 units depending on the part.
What engineering documentation do I need to send for a quick quotation?
Please provide your graphic overlay artwork (vector PDF, AI, or CorelDraw), circuit schematic/layout (Gerber RS-274X, DXF, or DWG), dome tactile requirements, connector pinout specifications, and target quantities. If your project includes PCBA backplanes, please include a complete BOM with manufacturer part numbers.
Can you integrate backlighting, displays, and embedded LEDs into the keypad?
Yes. We incorporate surface-mount LEDs directly into the spacer layer, embed clear or smoked display windows for LCD/OLED modules, and offer LED backlighting, fiber-optic mesh, or electroluminescent (EL) foils to ensure clear nighttime visibility.
How are deliveries handled for clients based in the All Saints region?
We ship via express air freight (DHL, FedEx, UPS) directly from our Shenzhen facility, with delivery times usually ranging between 5 to 8 business days once manufacturing and testing are complete. All orders ship in ESD-shielded, moisture-barrier packaging.
Ready to Build Your Custom Interface or Sensor Assembly?
Connect with our Shenzhen engineering desk for a comprehensive Design-for-Manufacture (DFM) review and an exact quote within 24 hours.
Contact Us