Piezo Transducer
Explore high-reliability hardware engineered for maritime resilience, high-humidity processing, and South Pacific industrial applications.
Global Exporting Track Record
Verified Buyer Rating Score
Flexible Turnkey Prototype MOQ
Engineering & Production Staff
Operating human-machine interface (HMI) systems and industrial control switchgear within Tonga presents distinct physical engineering challenges. Situated in the South Pacific convergence zone, the Kingdom experiences sustained relative humidity levels regularly exceeding 85%, continuous airborne sodium chloride aerosol exposure, and elevated equatorial ultraviolet radiation indexes (UVI 11+). Conventional off-the-shelf membrane keypads fabricated with basic polyester (PET) or standard commercial polycarbonates suffer premature catastrophic failure under these conditions, manifesting as conductive silver migration, spacer adhesive delamination, graphic embrittlement, and internal contact oxidation.
When selecting membrane switch panels and integrated control electronics for projects across Tongatapu, Vavaʻu, Haʻapai, and the outer islands, procurement managers and lead systems integrators must balance low initial prototyping costs against life-cycle mean time between failures (MTBF). Shenzhen Mivo Electronics provides end-to-end original design manufacturing (ODM) and original equipment manufacturing (OEM), bridging the technical gap between bare circuit fabrication, turnkey PCBA, and sealed outer human interfaces designed specifically for tropical maritime exposure.
A critical engineering failure observed in maritime HMIs deployed around Nukuʻalofa Harbor and inter-island ferry monitoring gear is the deployment of consumer-grade polycarbonates for front graphic overlays. UV-A and UV-B exposure quickly breaks the polymer bonds, causing yellowing, micro-cracking, and eventual seal rupture. Mivo Electronics utilizes textured biaxially-oriented Autotex XE Polyester films combined with multi-layer screen-printed UV blockers. This material formulation maintains tensile resilience, prevents chemical degradation from standard biocidal cleaners, and prevents yellowing over years of direct sunlight exposure.
| Performance Characteristic | Commercial Grade (Standard Polycarbonate) | Mivo Maritime Grade (Autotex XE PET + 3M 300LSE) | Operational Impact in Tonga |
|---|---|---|---|
| Direct Solar UV Resistance | Rapid yellowing and embrittlement within 6–12 months | Certified 1,000+ hours accelerated UV (ASTM G154) | Vital for open-deck fishing vessel telemetry and solar pump controllers |
| Moisture Ingress Protection | IP40 – IP54 (standard perimeter pressure adhesives) | IP65 to IP67 sealed continuous gasket enclosure | Prevents condensation shorts during high humidity and tropical storms |
| Conductive Trace Protection | Uncoated silver flake ink (susceptible to dendrite growth) | Carbon-overprinted silver tracks with dielectric passivators | Eliminates silver migration caused by salt-fog electrical conductivity |
| Adhesive Shear Strength | Standard acrylic glue (debonds under sustained heat/humidity) | 3M 300LSE / 467MP high-surface-energy adhesive systems | Resists peel stresses on powder-coated steel and aluminum chassis |
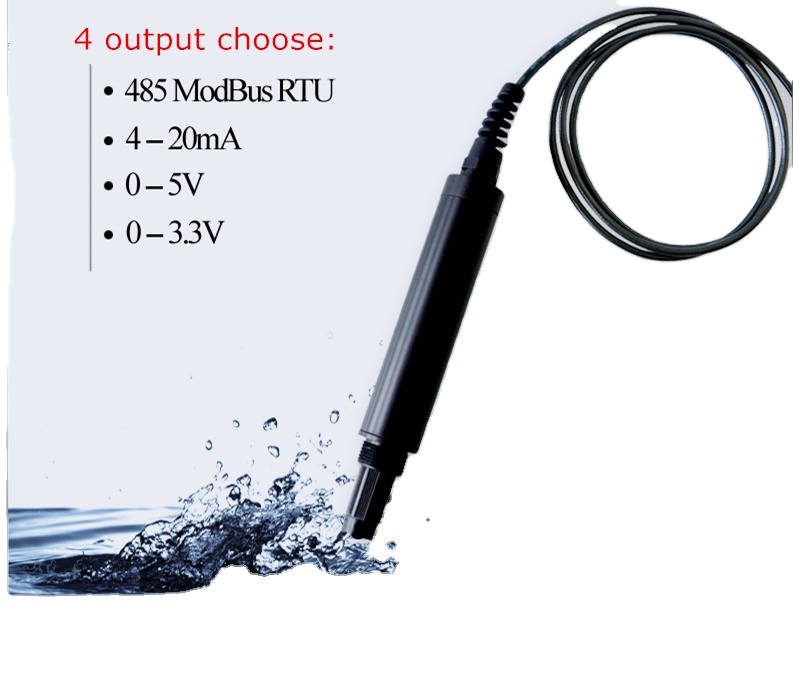
Membrane panels do not function in isolation; they serve as the front line of command for intricate internal electronic assemblies. Shenzhen Mivo Electronics delivers a true one-stop manufacturing advantage. By fabricating the bare circuit board (multilayer rigid FR-4 or aluminum core PCB), mounting active microcontrollers and SMD components, and mating the finished PCBA to an IP67 membrane switch overlay with tactile metal snap domes, we eliminate multi-vendor interface mismatches. Whether your application requires localized water turbidity telemetry via RS485 Modbus, high-precision thermal monitoring with PT100 RTD sensors, or ultrasonic liquid volume calculations in municipal sewer basins, our Shenzhen-based onsite-verified facility handles the entire value chain from initial Gerber and BOM review to final box-build packaging.
Customized membrane switches and industrial electronic sub-assemblies built to withstand local maritime and municipal environments.
Tonga's deep-sea tuna longline and artisanal reef vessels demand IP67-rated wheelhouse instrumentation panels, sonar trigger units, and bilge alert interfaces that resist continuous ocean spray, diesel oil splash, and heavy mechanical actuation.
Vanilla curing chambers, squash sorting automation, and root-crop washing operations across Tongatapu require wipe-down membrane overlays compatible with sanitizers, coupled with pierce-type PT100 temperature probes for batch control.
As outer islands migrate to autonomous photovoltaic-diesel hybrid microgrids, high-temperature-rated membrane control interfaces ensure battery storage modules, invertors, and pumping systems remain field-programmable without enclosure leaks.
Strategic technological evolutions driving human-machine interface requirements across island economies.
To combat climate vulnerability and sea-level rise affecting groundwater lenses, Tonga is installing small-scale reverse osmosis plants across outer atolls. These facilities require membrane control panels paired with DTS-600 turbidity transducers and DOS-600 dissolved oxygen sensors that operate without failure in hyper-saline pump rooms.
Traditional mechanical switches are giving way to capacitive membrane sensors that feature zero moving mechanical parts. By using complete continuous non-porous glass or chemically strengthened acrylic overlays, these interfaces completely eradicate the threat of dust, fine coral sand, and airborne salt crystallization entering the switch cavity.
Because international freight logistics to Tonga can incur high lead times, engineering teams are transitioning toward standardized connector tails (such as 2.54mm pitch female Berg or Nicomatic housings). Mivo's flexible minimum order quantities (starting from 5 pieces) allow utility engineers to hold critical replacement overlays on-island affordably.
Direct engineering oversight from China's premier hardware hub, eliminating trading middlemen and markup.
Unlike trading entities, our Shenzhen plant is onsite-checked and legally validated. Spanning our dedicated production floor in Yuanshan Street, Shenzhen, we integrate precision silk-screening, laser cutting, SMT high-speed placement lines, and testing equipment under ISO quality standards.
We do not merely print switch overlays; we build the intelligence behind them. From multilayer FR-4 circuit boards and aluminum core MCPCBs to complete component sourcing and firmware programming, our clients receive plug-and-play modules ready for final enclosure assembly.
We respect development timelines and understand the risks of heavy capital outlay. We support engineers and hardware startups with prototype PCBA and membrane switches from as low as 5 pieces, backed by full DFM (Design for Manufacturability) file reviews prior to production initiation.
Addressing engineering specifications, international freight logistics, and component customization.
Whether you require a salt-mist proof keypad prototype for marine equipment or volume turnkey PCBA manufacturing, Mivo's engineering group in Shenzhen is ready to review your files.