Integrated Membrane Switches & Sensor Solutions
Combining rugged human-machine interface assemblies with field-tested environmental, fluid, and mechanical monitoring sensors optimized for continuous operation in Jamaica's demanding Caribbean climate.
Membrane Switch Architecture: Engineering for High Humidity & Heavy Washdown
Industrial operations throughout Spanish Town—ranging from sugar refining and rum blending to pharmaceutical packaging and industrial chemical processing—demand control interfaces that withstand extreme humidity, caustic cleaning fluids, abrasive dust, and high thermal cycling. Standard off-the-shelf pushbuttons frequently fail due to corrosion along contact points and compromised ingress gaskets.
Shenzhen Mivo Electronics designs and manufactures multi-layered, hermetically sealed custom membrane switch interfaces. By integrating premium graphic overlays like MacDermid Autotex XE (UV-stabilized polyester) with screen-printed conductive silver inks and micro-dielectric barriers, our assemblies achieve true IP65, IP67, and IP68 environmental protection.
Furthermore, our Shenzhen facility pairs custom membrane keyboards directly with rigid FR-4 backplanes, Aluminum Core PCBs (MCPCB), or Flexible Printed Circuits (FPC), accommodating embedded surface-mount LEDs, optical clear display windows, capacitive touch ICs, and back-mounted RS485/Modbus telemetry modules.
| Parameter | Standard Specification |
|---|---|
| Overlay Material | Autotex PET / Polycarbonate (0.125mm - 0.25mm) |
| Circuit Layer | Screen-printed Silver / Carbon Ink or FPC Copper |
| Contact Resistance | < 100 Ω (Trace length dependent) |
| Dielectric Strength | 1,500 VDC Breakdown Threshold |
| Actuation Force | 250g to 450g (Tactile Metal Dome) |
| Operating Temp | -40°C to +85°C Continuous Range |
| Humidity Resistance | 95% RH at 60°C (Non-condensing) |
| Ingress Rating | IP65, IP67, NEMA 4X Hermetic Perimeter |
Mission-Critical Applications Across Spanish Town's Industrial Corridor
Spanish Town stands as the manufacturing capital of St. Catherine, Jamaica, hosting pivotal production plants along the Spanish Town Commercial Corridor, Salt Pond Road, and the Rio Cobre industrial valley. Here is how our custom HMI switches integrate directly into local processing lines.
Food, Beverage & Rum Bottling Facilities
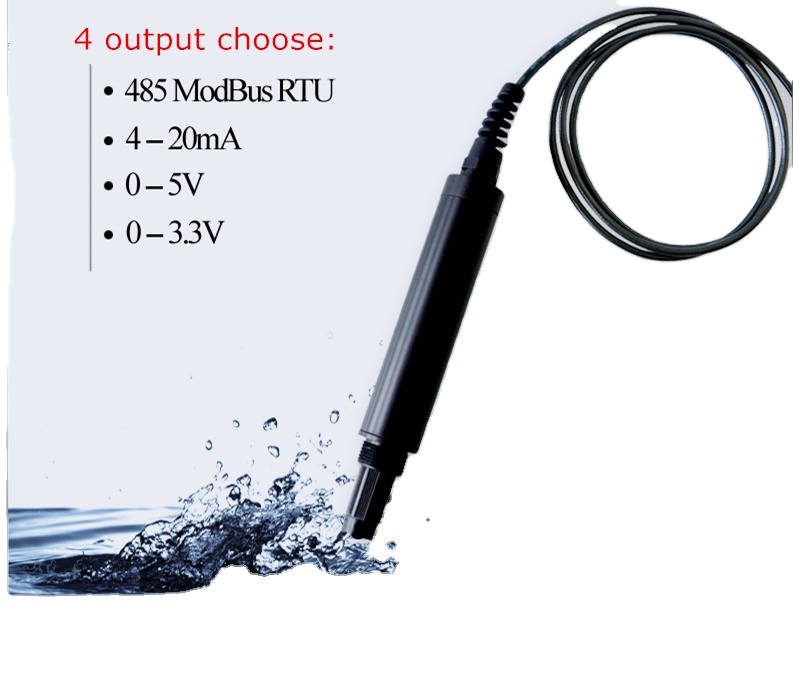
Sugar cane processing, rum blending, condensed milk, and citrus beverage facilities in St. Catherine demand rigorous Clean-in-Place (CIP) hot-chemical washdowns. Our chemically inert Autotex PET overlays withstand chlorine, citric acid, and sodium hydroxide washdowns while our DTS-600 turbidity sensors monitor wastewater compliance.
Pharmaceutical Formulation & Cleanrooms
Jamaica's domestic medical supply manufacturers around Spanish Town mandate sterile, dust-free front control panels with zero crevices where bacterial micro-contaminants can lodge. We provide completely flat, antimicrobial-treated surface overlays integrated with SHT30/31 cleanroom climate telemetry.
Corrugated Packaging & Paper Manufacturing
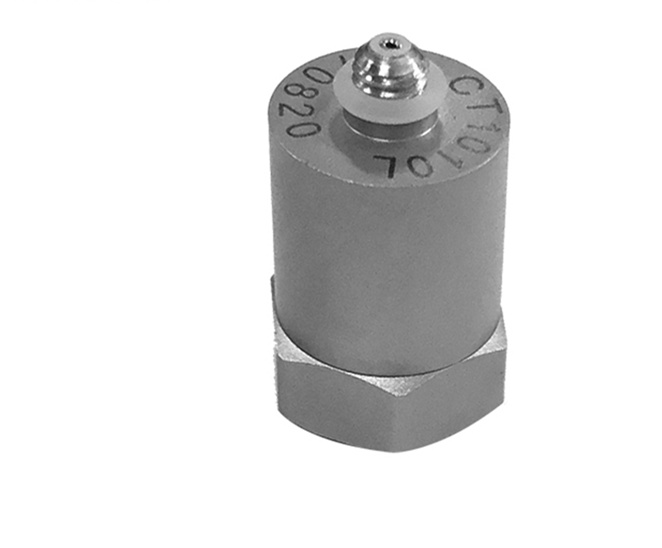
Heavy packaging plants operating along the corridor produce intense mechanical vibration and continuous fibrous dust. Our tactile metal-dome membrane switches deliver reliable feedback under high cycle frequencies without contact bounce, while CT1010L accelerometers trace conveyor bearing wear.
Emerging HMI Trends in the Jamaican Industrial Landscape
As manufacturing facilities in St. Catherine modernize under regional Industry 4.0 initiatives, procurement teams in Spanish Town are shifting from legacy electromechanical buttons toward unified, intelligent interface modules.
Industrial Transition Matrix: Spanish Town
IP67 Sealed Tactile Membrane Switches
Replacement of leaky mechanical pushbuttons with hermetically sealed tactile keypads to stop moisture ingress during tropical storms and plant washdowns.
Hybrid HMI Panels with Display Windows
Integration of optically clear anti-glare display windows for OLED/TFT readouts directly inside the membrane switch structure with back-mounted PCBA.
Sensor-Fused Intelligent Touch Surfaces
Capacitive touch combined with digital telemetry (RS485 Modbus, CANbus) transmitting temperature, turbidity, and vibration signals over a unified wiring harness.
Why St. Catherine Modernization Favors China Direct Sourcing
Procuring custom human-machine interfaces through regional third-party intermediaries often introduces lead times of 12 to 18 weeks and markups exceeding 200%. For plant engineers in Spanish Town striving to avoid costly production line shutdowns, direct collaboration with an onsite-verified Shenzhen manufacturer delivers distinct advantages:
- Rapid Tooling Turnaround: Custom graphic dies, embossing molds, and laser-cut adhesive gaskets finalized in 5 to 7 working days.
- Bespoke Environmental Customization: Tailored UV blockers, salt-fog inhibitors, and copper flex FPC substrates engineered to withstand the Jamaican maritime environment.
- One-Stop Turnkey Assembly: Simultaneous fabrication of bare circuit boards, surface mounting of microcontrollers and LEDs, and complete enclosure box-builds under one roof.
By bypassing multiple layers of brokers, Jamaican equipment operators preserve vital capital expenditure while gaining direct access to Shenzen Mivo's electrical and mechanical design engineering staff.
Why Global Buyers & Caribbean Operations Partner with Mivo
Headquartered in the global electronics capital of Shenzhen, China, Shenzhen Mivo Electronics Co., Ltd. combines rigorous Japanese-standard quality control with the agile supply chain of the Greater Bay Area.
Onsite-Verified Factory
Our manufacturing facility and cleanrooms have passed comprehensive third-party onsite verifications, proving our legal standing, production facilities, and employee capacity (51–100 technicians).
Low Prototype MOQ
Unlike rigid volume factories, we initiate prototype membrane switch and turnkey PCBA orders starting from just 5 to 10 pieces. Perfect for custom equipment retrofits and field testing.
Full In-House Turnkey SMT
We do not simply print membranes—we manufacture multilayer FR-4 PCBs, aluminum core substrates, solder stencils, component sourcing, and through-hole/SMT assembly with full functional testing.
Direct Caribbean Logistics
Established air-express and maritime logistics lines directly serving Kingston Port and Norman Manley International Airport, with compliant customs documentation for swift clearance in Jamaica.
Frequently Asked Questions: Sourcing Membrane Switches for Spanish Town
Clear, transparent answers addressing tooling, climatic suitability, payment terms, and logistics for industrial procurement officers and automation engineers across Jamaica.
What files are required to initiate a custom membrane switch manufacturing quote?
How do your membrane switches perform against Jamaica's tropical heat and coastal salt air?
Can you incorporate LED backlighting, tactile domes, and display windows on the same panel?
What are the typical lead times for prototypes and production batches to Jamaica?
How does Shenzhen Mivo handle component obsolescence and BOM sourcing?
Do you offer waterproof sensors and cable harnesses to pair with our membrane switches?
Upgrade Your Industrial HMI Reliability in Spanish Town
Consult directly with Shenzhen Mivo's senior engineering team. Whether you need 5 custom prototypes for a factory floor retrofit or 10,000 units for an OEM production line, we offer fast turnaround, verified ISO-standard manufacturing, and factory-direct pricing.